Get in touch with Zejiang Paper Machinery Company

Paper is a thin sheet of non-woven cellulosic material. This guide covers both paper and paperboard; their commercial classification depends on grade and construction as well as grammage, which EN ISO 536:2020 measures in grams per square meter (g/m² or GSM). EN ISO 536:2020. Grammage is measured in grams per square meter. “Mills” form everyday paper products by draining a dilute suspension of fiber through a fine forming wire mesh (Oklahoma State University Extension FAPC-169). The wet mat is pressed and dried on steam-heated cylinders into a self-bonding paper web.
What Is Paper? Definition, Sheet Structure, and Historical Evolution
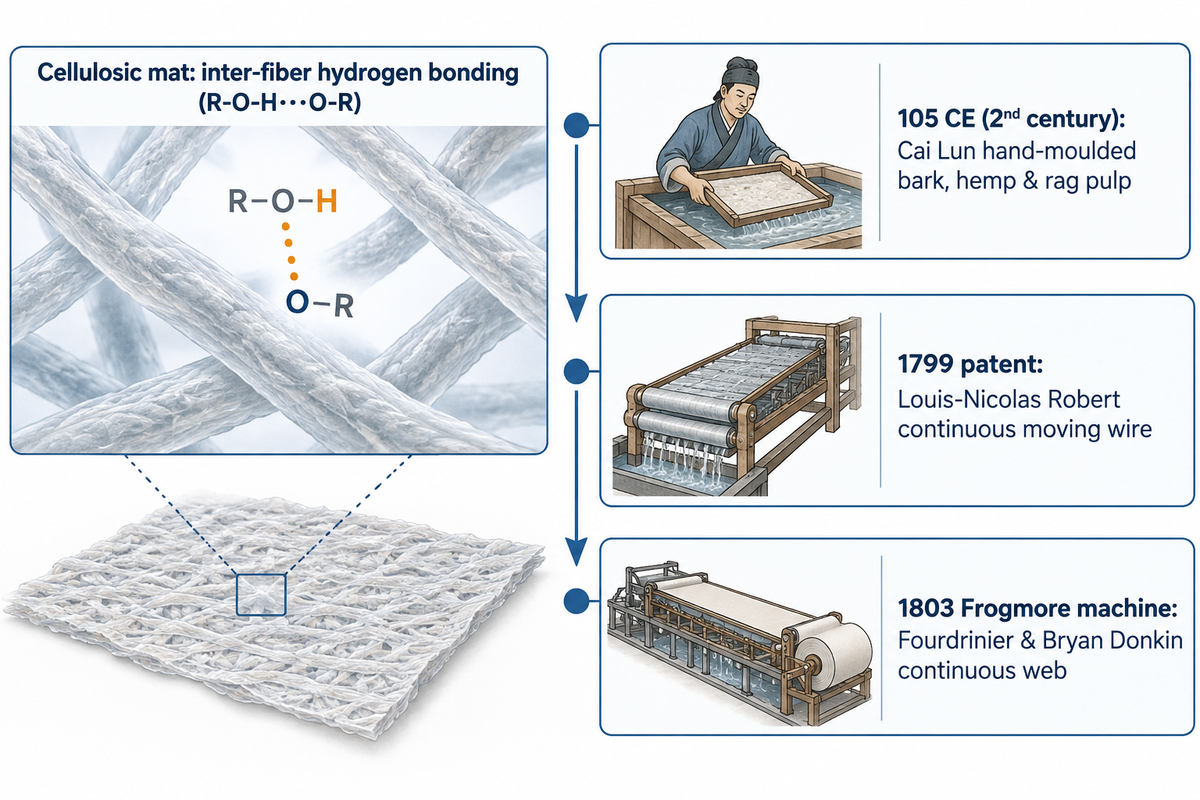
A sheet of paper is a thin, non-woven cellulosic mat held together by inter-fiber hydrogen bonding at the molecular level (R-O-H···O-R). It doesn’t need any synthetic adhesive to create a coherent web. When water drains and evaporates from beaten cellulose fibres, hydroxyl groups on adjacent walls come within nanometers of each other. They lock into a felted sheet. This random three-dimensional network separates true paper from ancient papyrus. Ancient artisans made that earlier writing material by pressing crossed strips of Cyperus papyrus pith without pulping.
Archaeological fragments show that the first paper sheets emerged in China before the Eastern Han court record. The court official Cai Lun is traditionally credited with reporting major improvements to papermaking in China in 105 CE during the 2nd century (Encyclopædia Britannica). His hand-moulded method macerated mulberry bark, hemp waste, old rag textiles, and fishing nets in water. Artisans then screened the pulp into a uniform sheet of fiber. By the 8th century, papermaking reached Baghdad, where workers operated linen and cotton rag stamping mills. The craft spread into Europe before the 15th century and supplied the durable substrate needed for movable-type printing presses.
Continuous base paper sheet manufacturing began in 1799 with the patenting of a continuous moving wire by Louis-Nicolas Robert (Encyclopædia Britannica). However, it was the first mechanized continuous papermaking machine financed by the Fourdrinier brothers and built by Bryan Donkin in 1803 that revolutionized the industry (Encyclopædia Britannica). The mid-19th century brought significant advances in mechanical groundwood and chemical wood pulping, enabling forest timber to replace scarce cotton rags. The craft spread into Europe before the 15th century and supplied the durable substrate needed for movable-type printing presses. Today, standard methods of test for papermaking are described by theEN ISO 536:2020 and other similar organizations.
What Is Paper Made Of? Cellulose Fibers, Pulps, and Chemical Additives
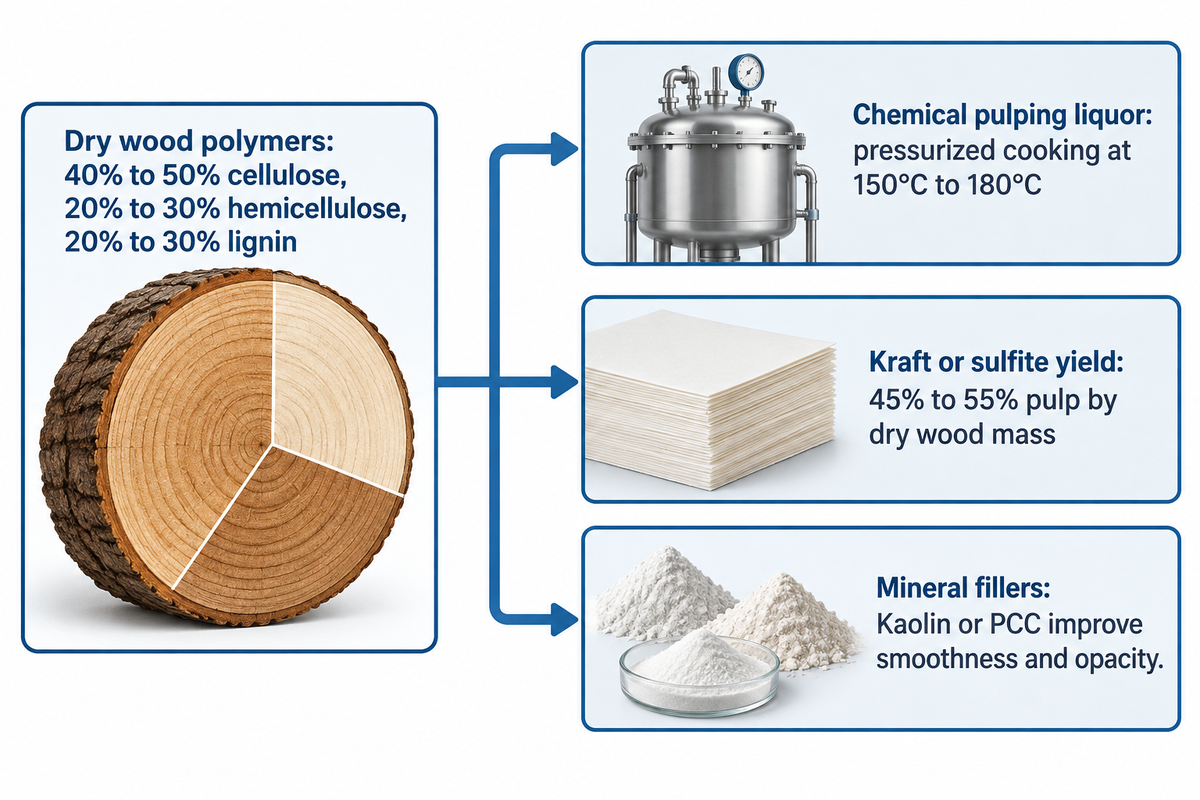
Paper uses cellulose fibers from wood, recovered paper, crop residues, or textiles, while raw wood is a lignocellulosic composite of three polymers. Dry wood contains 40% to 50% cellulose, 20% to 30% hemicellulose, and 20% to 30% lignin (Oklahoma State University Extension). Cellulose chains provide tensile strength and sheet flexibility. Hemicellulose promotes fiber swelling during refining. Lignin acts as a rigid natural binder that darkens and turns acidic under ultraviolet light. Mills separating pulp from wood must choose between high-yield mechanical processes and lignin-removing chemical treatments.
In mechanical pulping, logs or wood chips are ground against stones or refined into thermomechanical pulp (TMP) (Oklahoma State University Extension). This high-yield process retains most of the dry wood mass. Because lignin stays in the furnish, groundwood grades have high bulk and opacity, but yellow rapidly. In chemical pulping, wood chips are cooked in pressurized cooking liquor at 150°C to 180°C (Oklahoma State University Extension). Kraft or sulfite pulping dissolves much of the lignin and yields about 45% to 55% pulp by dry wood mass (NC State BioResources). That chemical pulp contains cellulose, hemicellulose, and residual lignin. Elemental chlorine free (ECF) chlorine dioxide stages then bleach the brown stock to the desired brightness.
Pulps and fillers are used to modify the furnish for printing paper to improve its printability. The total combination of all components in a given dry-mass basis should be 100% (NC State University BioResources). Fillers such as Kaolin or PCC improve smoothness and opacity. Chemical additives such as AKD or ASA enable better sizing. Buyers evaluating global paper pulp manufacturers for mill furnish sourcing verify both ash limits and alkaline sizing permanence before locking contracts.
What Materials Are Used to Make Paper Beyond Wood Pulp?
Aside from virgin softwood and hardwood lumber, mills process other materials such as recovered corrugated cartons, crop residues, textile fibers, and recovered paper. Recovered paper streams include old corrugated containers (OCC), mixed office waste, deinked newspapers, and other recovered paper. These furnishes supply a large proportion of the global papermaking furnish as recycled materials. The non-wood crops, such as bamboo, sugarcane bagasse, wheat straw, and reeds are fast growing. High-alpha-cellulose cotton linters, linen, and abaca hemp are also used for some specialized applications.
Major Types of Paper and Commercial Grade Classifications
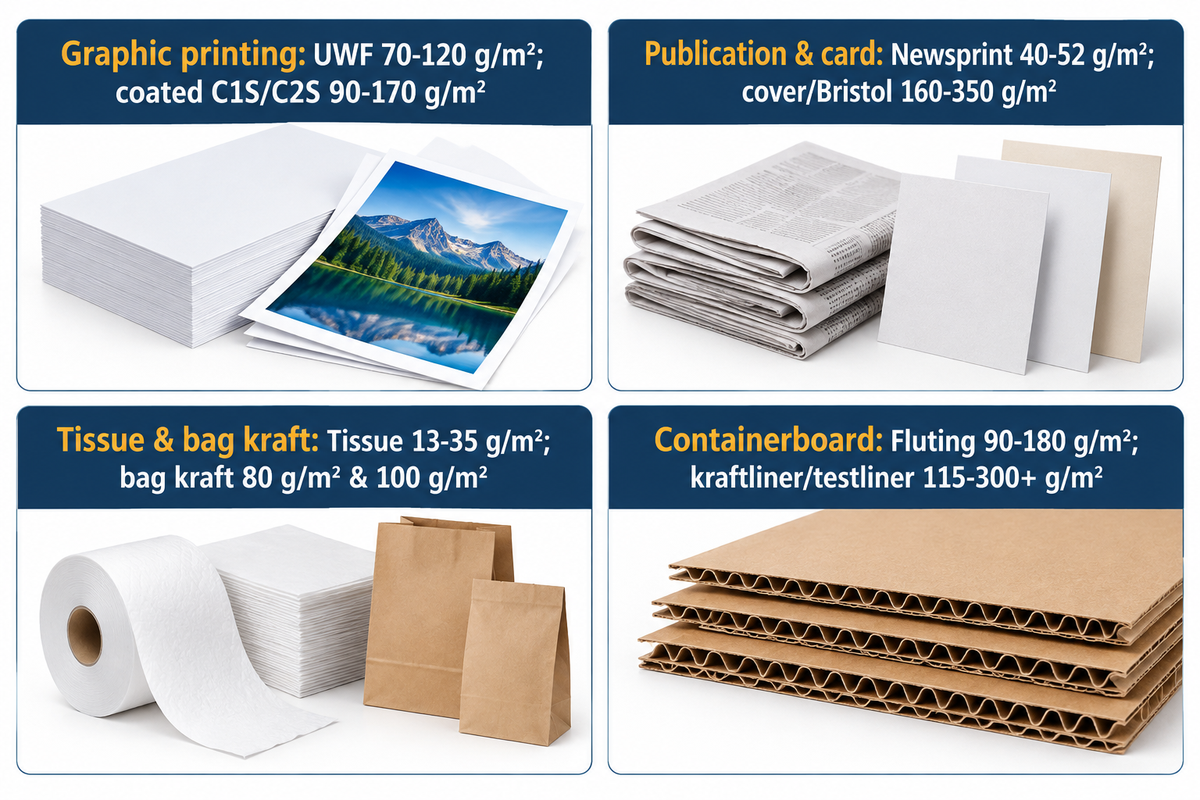
Industrial Buyers categorize different types of paper by paper weight, pulp chemistry, surface treatment and converting end use. Selecting the wrong commercial grade usually results in postal weights exceeding the limit and ink show through on high speed offset and digital presses. Commercial paper specifications distinguish nominal grammage, grammage tolerance and caliper because papers with the same grammage can have different thicknesses. Papers with the same grammage can have different thicknesses, so commercial paper specifications distinguish nominal grammage, grammage tolerance and caliper.
What Are the Main Types of Paper Used in Printing and Packaging?
The main types include uncoated woodfree bond and copy paper, coated art paper, newsprint, cover card stock, tissue, kraft paper, containerboard, and folding boxboard. In graphic printing, uncoated woodfree (UWF) rolls span 70–120 g/m², and pigment-coated C1S and C2S grades span 90–170 g/m² (Wikipedia). Newsprint spans 40–52 g/m², while cover or Bristol card stock spans 160–350 g/m² (Wikipedia; Hammer-IMS). In sanitary and packaging lines, tissue spans 13–35 g/m² (NC State BioResources), and carrier bag kraft is benchmarked across 80 g/m² and 100 g/m² sheets (PaperIndex Academy). Fluting medium spans 90–180 g/m², and kraftliner or testliner spans 115–300+ g/m² (Wikipedia). Uncoated woodfree bond and offset rolls serve everyday office printing. Coated art paper and studio drawing papers provide controlled ink holdout and surface area stability. The table below maps these commercial grades to their metric grammage, furnish, benchmarks, and uses.
| Commercial Grade | Typical GSM Range (g/m²) | Primary Furnish Base | Key Physical / Optical Benchmark | Primary Commercial Application |
|---|---|---|---|---|
| Sanitary Tissue Paper | 13–35 g/m² (NC State) | Virgin hardwood/softwood kraft or bamboo | Yankee creped bulk; high water absorbency | Facial tissue, bath rolls, kitchen towels, napkins |
| Newsprint | 40–52 g/m² (Wikipedia) | Mechanical TMP / groundwood + deinked pulp | High opacity at low GSM; rapid ink absorption | Daily newspapers, advertising flyers, inserts |
| Lightweight Coated (LWC) & Supercalendered (SC) | Grade-specific low-grammage publication web | Mechanical-pulp-based furnish; LWC is pigment-coated, while SC is uncoated and supercalendered | Smooth publication surface at low postal weight | High-circulation magazines, retail catalogs, inserts |
| Uncoated Woodfree (Bond / Copy) | 70–120 g/m² (Wikipedia) | Bleached chemical kraft + PCC or kaolin filler | 75 g/m² = 20 lb Bond; ±5% US GPO tolerance (Hammer-IMS) | Laser/inkjet office sheets, business forms, books |
| Coated Art Paper (C1S / C2S) | 90–170 g/m² (Wikipedia) | Bleached chemical pulp + clay/calcium carbonate coat | High ink holdout; gloss, silk, or matte finish | Magazines, brochures, luxury labels, art books |
| Heavyweight Cover, Card & Bristol | 160–350 g/m² (Wikipedia) | Bleached chemical kraft (single-ply or multi-ply) | High bending stiffness; requires creasing before folding | Catalog covers, business cards, index cards, tags |
| Studio Drawing & Cartridge | Grade-specific heavy sheet | Acid-free woodfree kraft or cotton rag blend | Controlled surface tooth; erasure durability | Technical sketching, illustration, watermedia |
| Sack & Bag Kraft Paper | 80 g/m² vs. 100 g/m² bag grades (PaperIndex) | Unbleached long-fiber softwood sulfate pulp | High tensile energy absorption (TEA) and tear | Multi-wall cement sacks, grocery carrier bags |
| Corrugating Fluting Medium | 90–180 g/m² (Wikipedia) | Semi-chemical hardwood (NSSC) or 100% OCC | High Concora medium flat crush resistance | Fluted core layer inside corrugated board |
| Kraftliner & Testliner | 115–300+ g/m² (Wikipedia) | Virgin softwood kraft or multi-ply recovered OCC | Specify liner properties separately; assess finished corrugated board ECT under ISO 3037 | Inner and outer facings of shipping cartons |
| Folding Boxboard (FBB) | 225–350+ g/m² (Wikipedia) | Multi-ply mechanical pulp core with bleached chemical outer plies | High bending stiffness and scoring foldability | Retail folding cartons, cosmetics and pharmaceutical boxes |
| Metallized & Dispersion Barrier Paper | Grade-specific flexible packaging web | Calendered virgin base + aqueous dispersion or metallized coat | Specify WVTR and OTR for the selected barrier structure and test conditions (Packaging Digest) | Heat-sealable food wraps, dry-mix pouches |
Packaging, Kraft, Tissue, and Specialty Paper Grades Compared
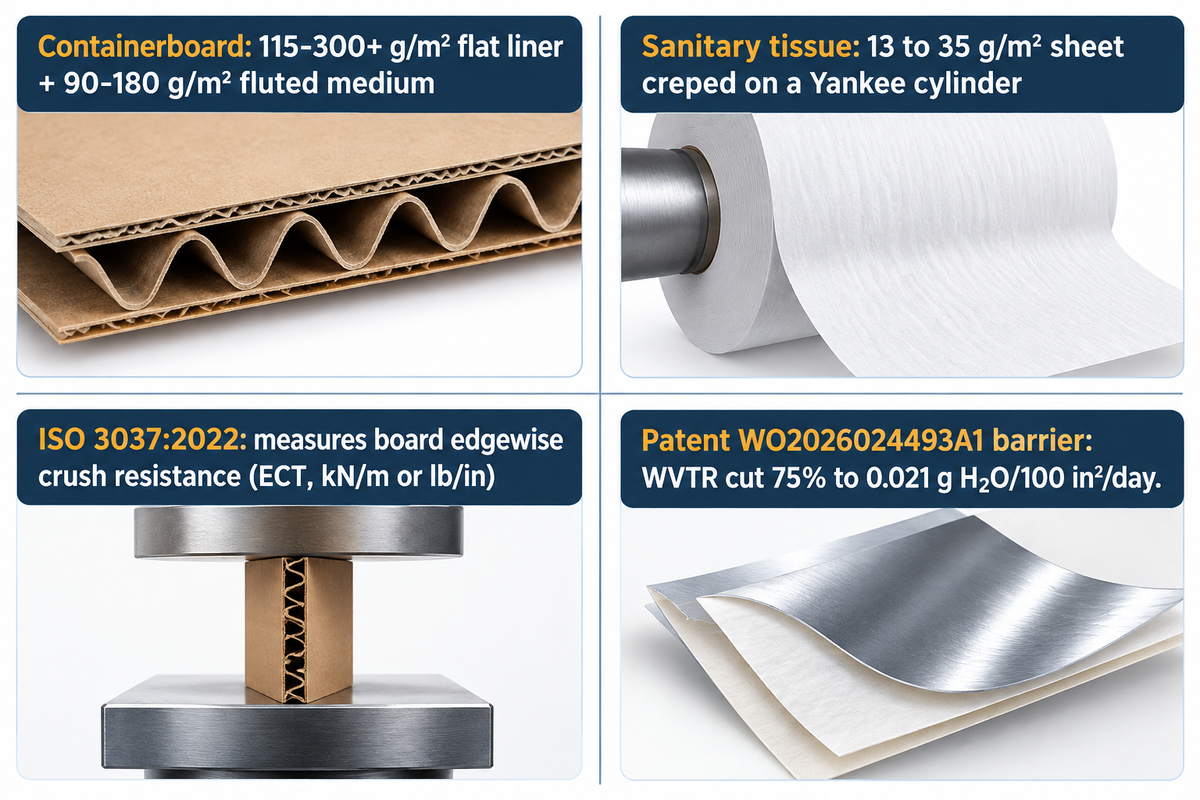
In recent years, the largest increases in consumption of paper and paperboard have been in packaging and sanitary products. For example, a flat liner with facings of 115-300+ g/m², in combination with a fluted corrugating medium of 90-180 g/m², makes up a group of containerboard grades. Virgin kraftliner retains long softwood fibers to resist bursting and humidity. In multi-ply forming, the competing recycled testliner relies on surface starch sizing. Henan Zejiang Paper Machinery Co., Ltd. provides kraft and corrugated paper machine lines which are configured to produce kraftliner, testliner and fluting medium.
Engineers must separate board-level edgewise crush resistance from whole-box stacking capacity when specifying corrugated board. ISO 3037:2022 measures the edgewise crush resistance (ECT, in kN/m or lb/in) of a corrugated fiberboard specimen loaded parallel to its flutes. By contrast, whole-box stacking survival of a filled carton is tested at the package level under ISO 12048:1994. In a warehouse stacking situation, box perimeter, board caliper and relative humidity affect board ECT.
At the opposite end of the grammage scale, sanitary tissue paper spans 13 to 35 g/m² (NC State BioResources). Instead of pressing for flat density, industrial tissue paper machine configurations use a doctor blade on a Yankee cylinder to crepe the sheet. Creping creates micro-folds that boost softness and water absorption. Meanwhile, food converters are adopting recycle-ready barrier webs (Packaging Digest). A metallized high-barrier paper food packaging structure in Patent WO2026024493A1 cut water vapor transmission rate (WVTR) by 75% to 0.021 g H2O/100 in²/day. Under the patent’s test conditions, oxygen transmission rate (OTR) also dropped by 90% to 0.0463 cc O2/100 in²/day.
Paper GSM, Basis Weight, Caliper, and Standard Sheet Sizes
Two competing measurement systems for paper product specifications—metric grammage and North American basis weight—often stall cross-border paper procurement. Comparing paper grades requires both their basis weight and the grade-specific reference sheet size. Paper grammage is mass per unit area, expressed in grams per square meter (g/m² or GSM). EN ISO 536:2020 and TAPPI T410 describe standard methods for determining it.
What Is the Difference Between GSM and Basis Weight in Paper?
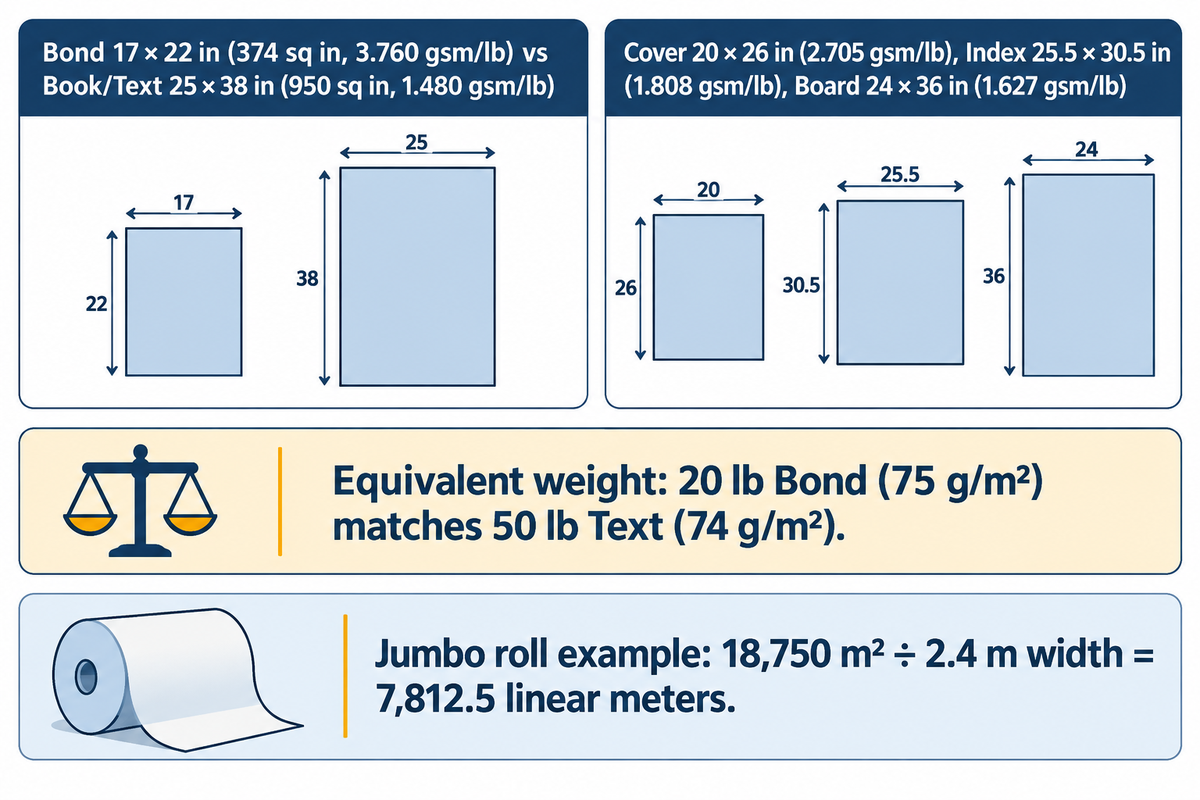
Metric GSM measures the mass of one square meter of any grade on a single scale, whereas North American basis weight measures the mass in pounds (lb) of 500 sheets cut to that grade’s uncut parent sheet size (Hammer-IMS). Converting the 5 major North American parent-sheet ream weight grades to metric GSM requires multiplying each pound rating by its parent-sheet area factor. Bond 17 × 22 in (374 sq in, 3.760 gsm/lb) and Book/Text 25 × 38 in (950 sq in, 1.480 gsm/lb) convert office and book grades (Hammer-IMS). Cover 20 × 26 in (520 sq in, 2.705 gsm/lb), Index 25.5 × 30.5 in (777.75 sq in, 1.808 gsm/lb), and Board 24 × 36 in (864 sq in, 1.627 gsm/lb) convert to metric GSM under TAPPI T410 and EN ISO 536:2020 (Hammer-IMS). As a result, 20 lb Bond (75 g/m²) and 50 lb Text (74 g/m²) have nearly identical metric weight.
“The most prevalent mistake: assuming 80 lb cover and 80 lb text are the same weight. A 20 lb Bond sheet and a 50 lb Text sheet both measure approximately 74–75 GSM despite their different pound ratings.”
| North American Grade & Weight | Uncut Parent Sheet Size (in) | Single Sheet Area (sq in) | Exact Multiplier (gsm/lb) | Metric Grammage (g/m²) |
|---|---|---|---|---|
| 20 lb Bond / Ledger / Copy | 17 × 22 in | 374.0 sq in | 3.760 gsm/lb | 75.2 g/m² (standard 75 GSM, Hammer-IMS) |
| 24 lb Bond / Laser | 17 × 22 in | 374.0 sq in | 3.760 gsm/lb | 90.2 g/m² (standard 90 GSM, Hammer-IMS) |
| 50 lb Book / Text / Offset | 25 × 38 in | 950.0 sq in | 1.480 gsm/lb | 74.0 g/m² (matches 20 lb Bond, Hammer-IMS) |
| 60 lb Book / Text / Offset | 25 × 38 in | 950.0 sq in | 1.480 gsm/lb | 88.8 g/m² (matches 24 lb Bond, Hammer-IMS) |
| 70 lb Book / Text | 25 × 38 in | 950.0 sq in | 1.480 gsm/lb | 103.6 g/m² (standard 105 GSM, Hammer-IMS) |
| 65 lb Cover Cardstock | 20 × 26 in | 520.0 sq in | 2.705 gsm/lb | 175.8 g/m² (standard 176 GSM, Hammer-IMS) |
| 80 lb Cover Cardstock | 20 × 26 in | 520.0 sq in | 2.705 gsm/lb | 216.4 g/m² (standard 216 GSM, Hammer-IMS) |
| 90 lb Index Bristol | 25.5 × 30.5 in | 777.75 sq in | 1.808 gsm/lb | 162.7 g/m² (standard 163 GSM, Hammer-IMS) |
| 110 lb Index Bristol | 25.5 × 30.5 in | 777.75 sq in | 1.808 gsm/lb | 198.9 g/m² (standard 199 GSM, Hammer-IMS) |
| 100 lb Tag / Board | 24 × 36 in | 864.0 sq in | 1.627 gsm/lb | 162.7 g/m² (standard 163 GSM, Hammer-IMS) |
Worked Example, Jumbo Roll Linear Length & Sheet Conversion: Suppose a converter orders a 1,500 kg jumbo parent roll of 80 g/m² uncoated offset paper with a 2,400 mm (2.4 m) trim width. Total web area equals 1,500,000 g divided by 80 g/m², which yields 18,750 m². Dividing 18,750 m² by the 2.4 m roll width gives 7,812.5 linear meters of continuous web. When sheeting into ISO 216 A4 size (210 × 297 mm, √2:1 aspect ratio) or North American Letter size (8.5 × 11 in), converters check caliper thickness and machine direction versus cross direction paper grain. Converters generally orient critical folds parallel to the paper grain and use suitable creasing to reduce cracking, especially in heavier or coated stocks (PrintPlanet Forum).
Virgin Kraft vs. Recycled Fiber vs. Non-Wood Pulp Performance
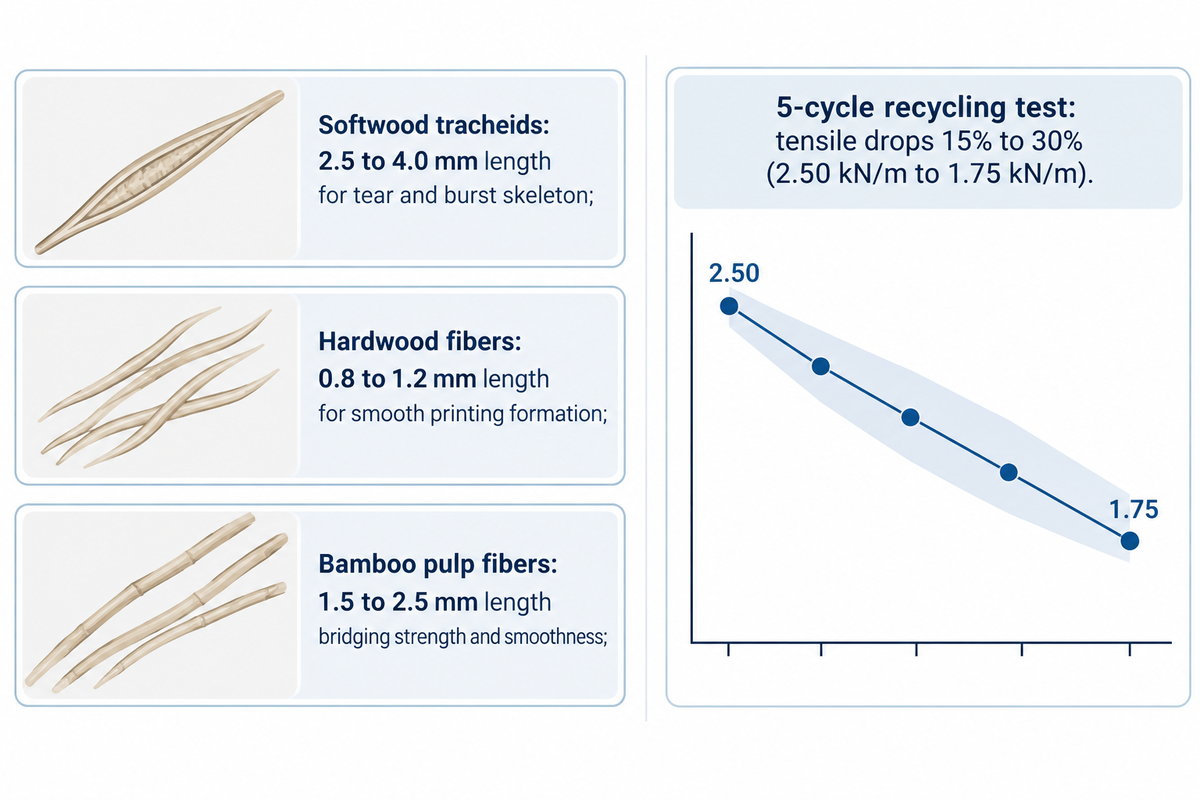
Selecting between virgin softwood kraft, virgin hardwood kraft, recycled paper, and non-wood bamboo or sugarcane bagasse requires comparing their fiber morphology, sheet strength and recycling life. Softwood tracheids average 2.5 to 4.0 mm in length and form a strong skeleton for tear and burst resistance (NC State BioResources). Hardwood fibers average 0.8 to 1.2 mm and fill surface voids for smooth printing (NC State BioResources). Bamboo pulp fibers span 1.5 to 2.5 mm, bridging softwood strength and hardwood formation. In laboratory handsheet trials (Journal of Natural Fibers 2023), adding 2.50 wt% bamboo pulp to recycled wood-pulp furnish restored tensile strength above the unblended recycled paper control. For tissue production, World Paper Mill reports bamboo furnish drying energy at 700–800 kWh/t versus roughly 1,000 kWh/t for wood pulp under its compared conditions. Sugarcane bagasse offers shorter agricultural fibers for printing, tissue, and corrugating in areas where timber is scarce. However, high-tear packaging grades typically blend bagasse with long-fiber kraft, and direct multi-cycle recycling curves for bagasse are not standardized in the referenced studies.
How Many Times Can Paper Fibers Be Recycled Before Losing Strength?
Repeated recycling reduces fiber bonding and sheet strength, so mills add virgin fibers to recycled furnish to meet strength targets and replace processing losses (U.S. EPA). Virgin reinforcement is adjusted by grade rather than triggered by a fixed cycle count (Springer Journal of Material Cycles and Waste Management 2025). Two physical mechanisms govern this degradation. First, retained fibers undergo irreversible cell-wall hornification, which drops sheet strength most sharply during the first drying and rewetting cycle (Springer 2025). Second, washing and screening cause cumulative fines loss, and U.S. EPA consumer guidance notes an average recovery span of five to seven cycles.
In 5-cycle laboratory recycling tests of bamboo and wood chemical pulps (NIH PMC10137927), tensile strength dropped 15% to 30% (from 2.50 kN/m to 1.75 kN/m). Mills setting up a waste paper OCC recycling line use fractionating screens, refining control, and targeted virgin long-fiber or bamboo blending to offset hornification.
How Is Paper Made Step by Step Inside an Industrial Paper Mill?
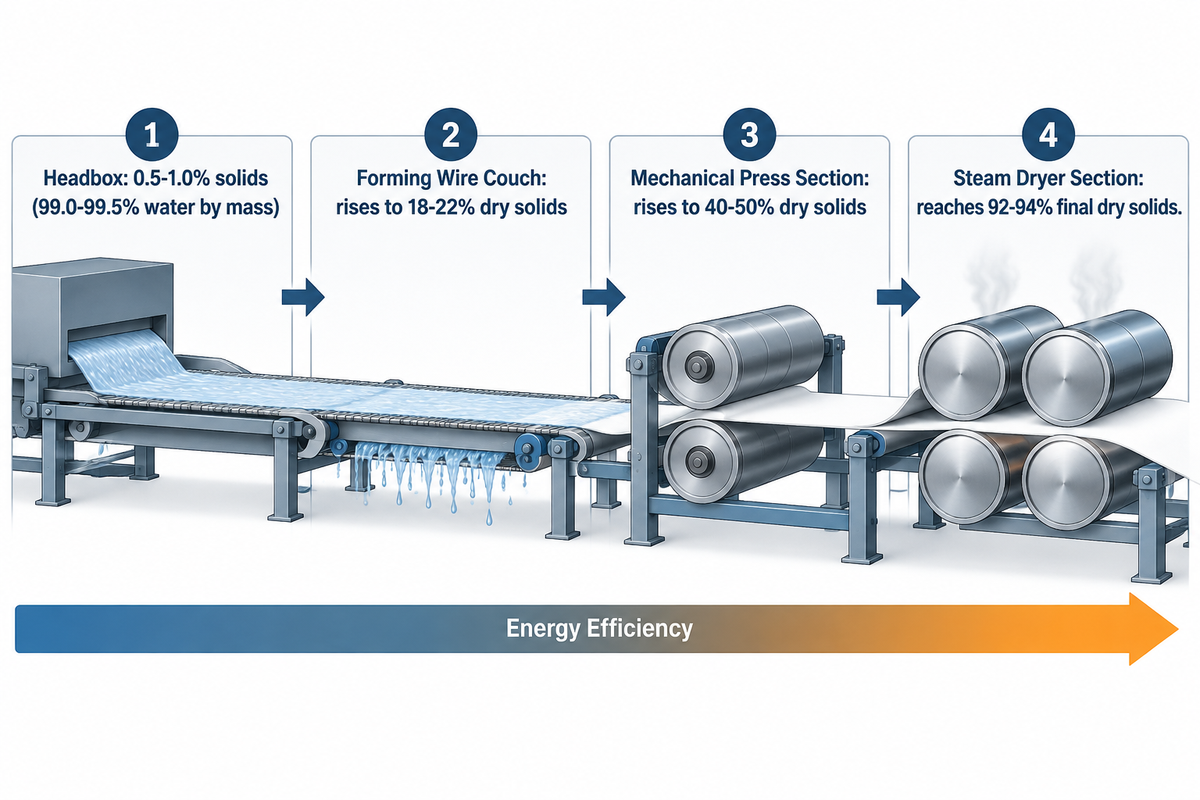
Industrial papermaking removes water sequentially by preparing the pulp stock, draining the dilute suspension through a wire mesh, pressing the wet mat, and drying it on steam cylinders (Oklahoma State University Extension FAPC-169). To make a profit when making paper, a mill has to maximize mechanical water removal prior to the sheet entering the steam dryer section.
How Is Paper Manufactured Step by Step From Pulp to Reel?
From pulp to reel, mills prepare the stock, form the sheet on a wire, press it, and dry it on steam-heated cylinders. Across the 4-stage dryness progression from headbox to reel, dry-mass fiber consistency rises across the Headbox (0.5–1.0% solids, or 99.0–99.5% water by mass), Forming Wire Couch (18–22% solids), Mechanical Press Section (40–50% solids), and Steam Dryer Section (92–94% solids) (Oklahoma State University Extension; NC State University BioResources). Pressing removes water mechanically with much less energy than evaporating it in the dryer section, so greater press-section dryness reduces steam demand (NC State University BioResources).
| Process Stage | Dry Solids In → Out (by Mass) | Primary Dewatering Mechanism | Core Mill Machinery & Components | Primary Process Control Target |
|---|---|---|---|---|
| 1. Stock Preparation & Refining | Thick stock diluted to 0.5%–1.0% solids (OSU FAPC-169) | White-water dilution & mechanical refining | Hydrapulper, disc/conical refiner with steel discs, SUS304/316L pressure screen | Freeness (°SR / CSF), fiber fibrillation, contaminant removal |
| 2. Headbox & Wire Forming Couch | 0.5%–1.0% solids → 18%–22% solids (NC State) | Gravity drainage & vacuum foil suction | Hydraulic/air-cushion headbox, endless synthetic wire mesh, suction couch roll | Jet-to-wire ratio, cross-direction basis weight profile |
| 3. Mechanical Press Section | 18%–22% solids → 40%–50% solids (NC State) | Mechanical nip compression into press felts | Roll press or extended-nip shoe press, press felts, suction press rolls | Nip linear load (kN/m), sheet consolidation, felt permeability |
| 4. Steam Dryer Section | 40%–50% solids → 92%–94% solids (NC State) | Steam-heated thermal evaporation | Multi-cylinder steam-heated dryer cans or Yankee cylinder, hood heat recovery | Steam pressure, pocket ventilation, target equilibrium moisture |
| 5. Size Press & Coating | Dry web re-wetted with starch/pigment and re-dried | After-dryer thermal evaporation | Pond or film metering size press, blade/curtain coater, infrared/air-turn dryers | Surface starch pickup (g/m²), Cobb60 water absorptiveness |
| 6. Calendering, Reel-Up & Rewinding | 92%–94% solids locked at Pope reel | Mechanical nip finishing | Hard/soft nip calender stack, Pope reel, high-speed slitter rewinder | Caliper uniformity, Sheffield smoothness, parent roll hardness |
In stock preparation, grooved steel discs fibrillate fiber walls expand bonding area, explaining how the pulp refining process develops fiber bonding. Downstream SUS304 and SUS316L slotted and drilled pressure screen baskets remove stickies and shives. At the wet end, stainless steel open, air-cushion, and hydraulic headboxes with micro-turbulence and dilution-water basis-weight profiling spread the diluted fiber suspension onto the wire to form paper evenly. At unchanged dry-fiber throughput, final moisture, and dryer efficiency, raising post-press dry solids leads to improved dryer performance, since less water needs to be evaporated and steam demands decrease. Therefore, the mills strive to balance press nip loading to improve water removal while avoiding bulk sheet crushing before the industrial paper drying process in the dryer section.
How Paper Machine Forming Sections Match Commercial Paper Grades
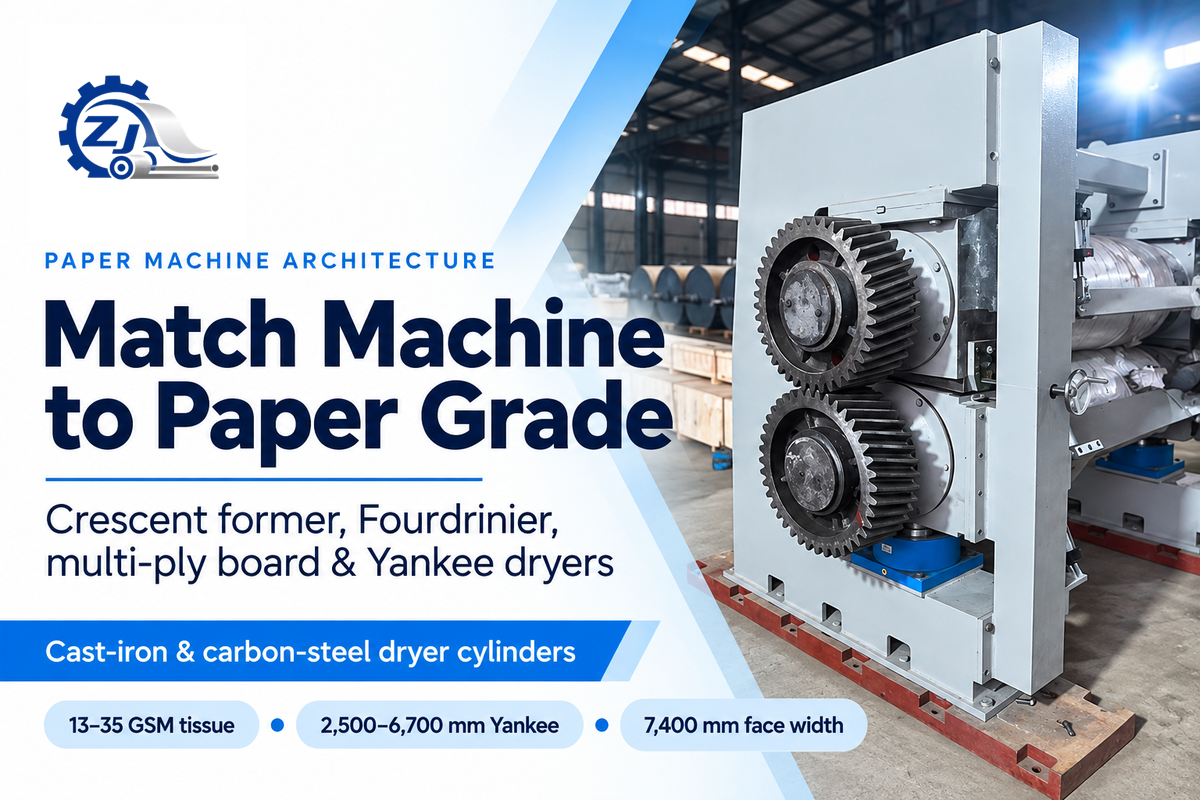
No single paper machine configuration can efficiently manufacture all commercial grades. For that reason, large OEMs, like Valmet, Voith, and ANDRITZ, build ultra-wide integrated lines. Smaller and specialty paper mills depend on specific forming architectures, in combination with their daily tonnage (TPD) and furnish freeness. Henan Zejiang Paper Machinery Co., Ltd. has paper machine platforms for tissue grades, including facial tissue, toilet tissue, kitchen towels, and napkins, in both single-cylinder mould and high-speed crescent former configurations. They also manufacture systems for forming, pressing, drying and the supercalendering process for smooth printing paper.
| Target Paper Grade | Forming Section Architecture | Recommended Headbox Type | Dryer Section Configuration | Primary Engineering Advantage |
|---|---|---|---|---|
| Facial, Toilet, Towel & Napkin Tissue (13–35 GSM) | Crescent Former or Single-Cylinder Mould | High-turbulence hydraulic headbox | Yankee dryer cylinder (2,500–6,700 mm diameter) + high-velocity hood | Direct felt-to-roll transfer eliminates open web draws at high speed |
| Uncoated Copy & Offset Printing (70–120 GSM) | Fourdrinier machine or Hybrid Gap Former | Air-cushion or hydraulic dilution headbox | Multi-cylinder cast-iron/carbon-steel dryers + film size press + calendering | Balanced two-sided smoothness and tight cross-direction GSM profile |
| Kraftliner & Testliner (115–300+ GSM) | Multi-wire Fourdrinier (2–3 forming wires) | Primary + secondary air-cushion/hydraulic headboxes | Heavy-duty multi-cylinder dryer groups + high-impulse shoe press | Separate forming layers allow mills to tailor ply strength and surface quality; kraftliner uses predominantly virgin kraft fiber, while testliner uses predominantly recovered fiber |
| Corrugating Fluting Medium (90–180 GSM) | Single Fourdrinier or Multi-Cylinder Vat | Open or air-cushion stainless steel headbox | Multi-deck steam dryer cylinders + starch size press | High starch penetration for Concora flat crush and board ECT |
| Multi-Ply Folding Boxboard (FBB, 225–350+ GSM) | Multi-Fourdrinier or Hybrid Multi-Ply Former | Individual ply hydraulic headboxes | Multi-cylinder dryer section + optional Yankee MG glazing cylinder + coating section | Folding boxboard typically combines a bulky mechanical-pulp middle layer with chemical-pulp outer layers for stiffness and print gloss |
| Recycled Greyboard & Chipboard | Multi-Cylinder Mould Vat Machine | Individual vat flow distributors | Multi-deck steam dryer cylinders (without Yankee MG glazing cylinder) | Greyboard commonly uses recovered fiber to form high-caliper rigid board across multiple cylinder vats |
| Specialty & Low-Speed Cultural Grades | Single-Wire Fourdrinier or Cylinder Mould | Open stainless steel headbox | Cast-iron steam dryer cans (face width up to 7,400 mm) | Low capital expenditure and rapid grade changeovers |
According to Henan Zejiang Paper Machinery Co., Ltd. dryer cylinder specifications, the company supplies cast-iron and carbon-steel paper machine dryer cylinders. It also engineers customizable Yankee dryer cylinders across a 2,500 mm to 6,700 mm diameter range and up to 7,400 mm face width.
Paper Quality Testing Standards, Bulk Pricing, and Mill Cost Drivers
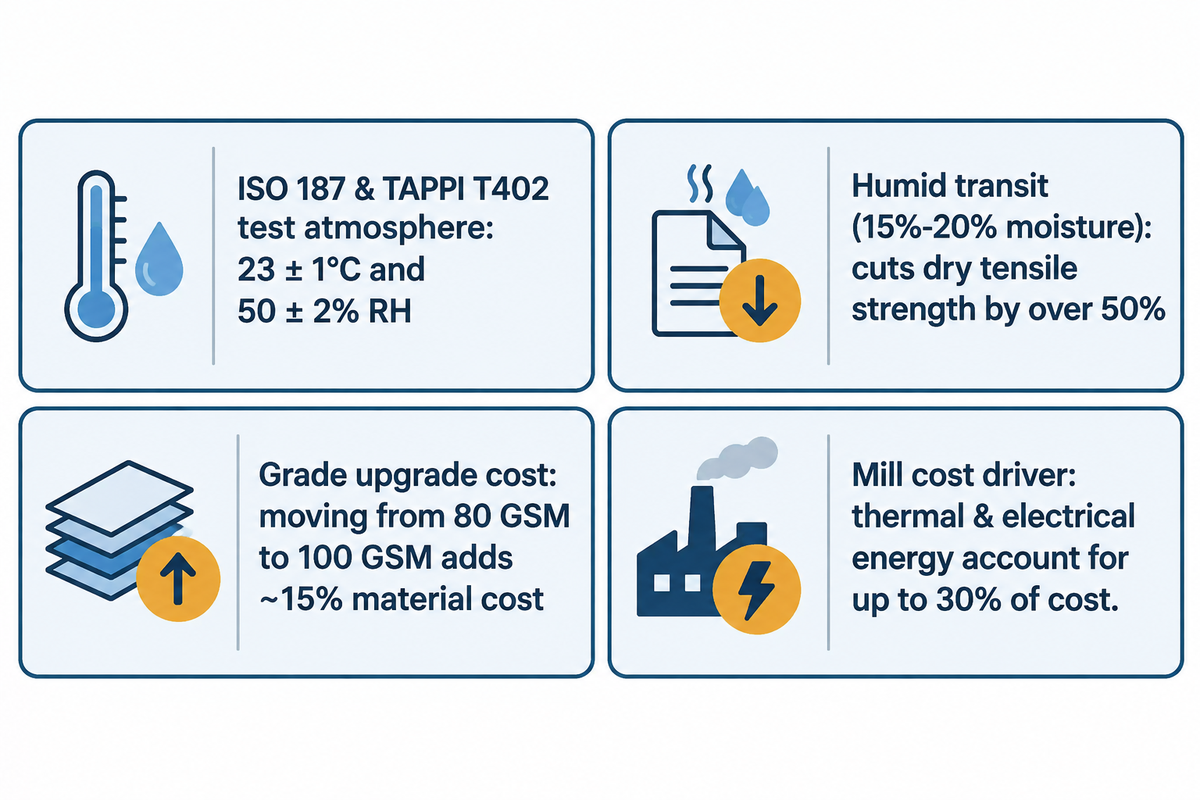
Writing “80 GSM paper” or “32 ECT board” on a purchase order without citing the test atmosphere invites quality disputes. For properties of paper, shifts in ambient humidity cause physical changes. As documented by PaperIndex Academy, sheet moisture of 15%–20% during humid transit cuts dry tensile strength by over 50%. Upgrading from 80 GSM to 100 GSM adds roughly 15% to material cost (PaperIndex Academy). Heavier sheets can still lose strength in humid warehouses; sizing limits liquid-water uptake, wet-strength chemistry improves strength after wetting, and moisture-controlled storage limits humidity exposure.
Buyers must separate two distinct moisture specifications: water absorptiveness and wet tensile strength. ISO 535:2023 (the Cobb60 test) measures the mass of water absorbed in g/m² over 60 seconds by sized paper and paperboard weighing at least 50 g/m². Mills control Cobb60 values using internal or surface sizing (AKD/ASA). Tensile strength after a wetting treatment is measured and compared to dry tensile strength. Wet-strength retention compares that wet result with dry tensile strength, and polyamide-epichlorohydrin (PAE) resin is commonly used to improve wet tensile strength.
Commercial roll pricing depends on regional pulp indexes, furnish blends, GSM, and reel trim width. Consequently, bulk per-ton paper prices are quote-based. To compare supplier quotes objectively, buyers evaluate the cost drivers of the mills. Pulp and fiber furnish represent the biggest cost component. Meanwhile thermal and electrical energy account for up to 30% of paper production costs (NC State University BioResources). Use the checklist below to lock acceptance criteria before issuing an RFQ.
6-Point Mill Specification Verification Checklist
- Condition sample sheets to moisture equilibrium and test them at 23 ± 1°C and 50 ± 2% relative humidity as defined in ISO 187 and TAPPI T402. If preconditioning is required, use a lower humidity conditioning atmosphere before standard conditioning.
- Specify target grammage (g/m²) and follow the specimen area, sampling, and weighing accuracy rules of EN ISO 536:2020 or TAPPI T410. Lock roll-to-roll tolerance within ±5% (US GPO standard).
- State maximum 60-second Cobb water uptake (g/m²) for sized grades weighing at least 50 g/m² under ISO 535:2023 and TAPPI T441. Specify PAE wet-strength retention separately if humid wetting is expected.
- Specify board-level edgewise crush resistance (ECT in kN/m per ISO 3037:2022) separately from filled-carton compression stacking load (ISO 12048:1994).
- Lock machine-direction (MD) versus cross-direction (CD) grain orientation (grain-long vs. grain-short) alongside target caliper thickness and reel trim width.
- Require valid FSC-STD-40-004 V3-1 or PEFC ST 2002:2020 chain-of-custody certificate numbers. Include HS Chapter 47 and Chapter 48 geolocation polygons for European Union shipments (Stibbe EUDR Analysis).
2026 Pulp and Paper Industry Outlook: Packaging Substitution and EUDR Compliance
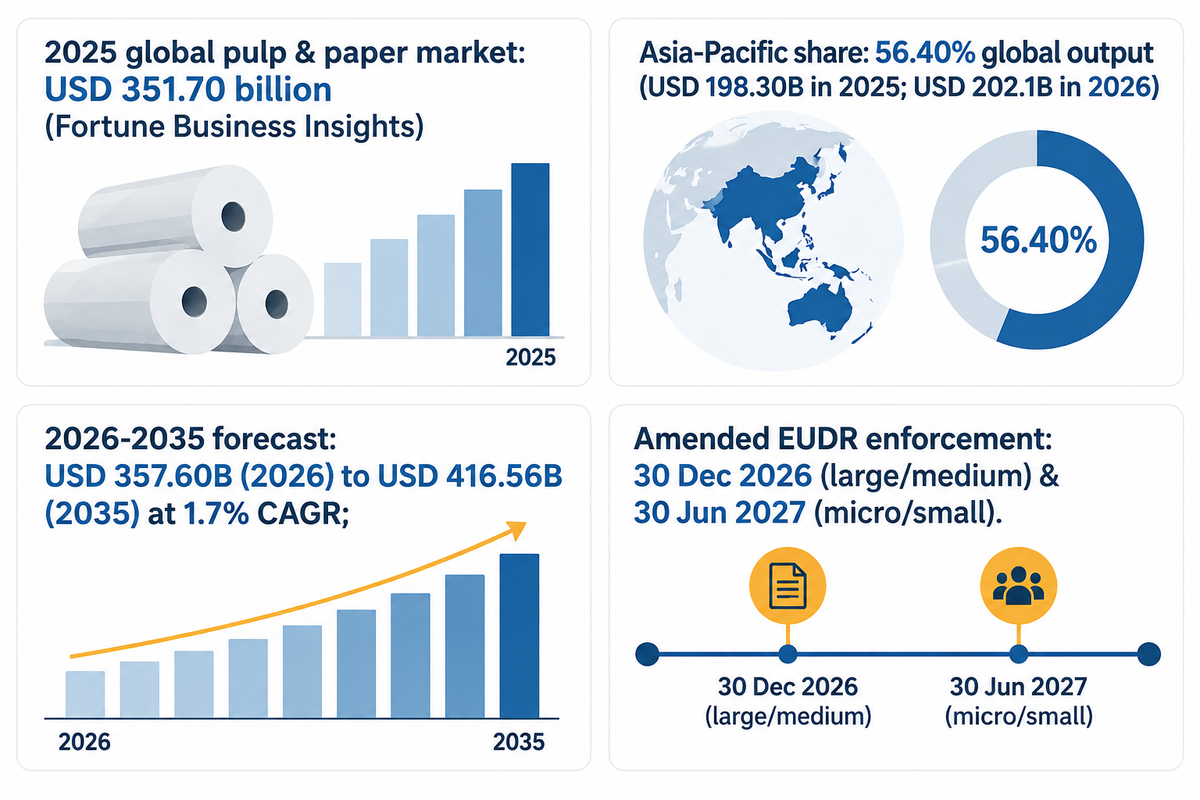
Global demand for paper is shifting from graphic newsprint toward e-commerce containerboard, sanitary tissue, and barrier wraps. According to Fortune Business Insights, the global pulp and paper market reached USD 351.70 billion in 2025. It’s projected to grow from USD 357.60 billion in 2026 to USD 416.56 billion by 2035 at a 1.7% CAGR. Asia-Pacific leads global output with a 56.40% market share (USD 198.30 billion in 2025 and USD 202.1 billion in 2026). North America accounts for USD 48.0 billion (Fortune Business Insights).
Compliance with regulations is transforming global fiber supply chains to zero deforestation. On 23 December 2025, the European Union published Regulation (EU) 2025/2650 amending the EU Deforestation Regulation (EUDR) (Stibbe legal analysis; European Commission). The amended regulations stipulate mandatory enforcement on large and medium operators on 30 December 2026, and on micro and small enterprises on 30 June 2027. Regulation (EU) 2025/2650 removed printed books, newspapers, and pictures under ex HS Chapter 49 from Annex I. However, wood pulp (HS Chapter 47) and uncoated/coated paper, kraftliner, paperboard, and cartons (HS Chapter 48) remain subject to plot-level geolocation traceability requirements.
Frequently Asked Questions About Paper
Why does paper turn yellow and brittle over time?
Paper turns yellow and brittle because lignin in mechanical wood pulp oxidizes to dark chromophores on exposure to ultraviolet light and air. Additionally, the historical use of alum-rosin sizing creates sulfuric acid, which cleaves cellulose polymer chains. Woodfree papers that use low-lignin, alkaline-buffered woodfree fibers resist yellowing and acid-driven embrittlement by removing lignin and chemically buffering the sheet with alkaline calcium carbonate ( NC State BioResources ).
Why does paper tear more easily in one direction than the other?
Paper torn parallel to the machine direction (MD) tears straighter because headbox jet shear aligns cellulose fibers parallel to the moving Fourdrinier wire. When paper is torn in the cross direction (CD), the tear path must pass through thousands of aligned fibers, and therefore isn’t as smooth. This creates a jagged edge, in contrast to a smooth edge on a tear in the machine direction.
What is the difference between coated and uncoated paper?
Uncoated paper’s porous cellulose fiber network is exposed after starch sizing. Coated paper has kaolin clay or calcium carbonate bound with latex sealing the network. Printing inks penetrate uncoated paper, resulting in a matte finish. Glossy grades are supercalendered to obtain a high gloss. Coating influences ink holdout and absorption for smooth and sharp halftone reproduction.
Is 20 lb bond paper the same as 75 GSM copy paper?
Yes. A 500-sheet ream of 20 lb North American Bond paper uses a 17 × 22 inch parent sheet size. Under TAPPI T410, that weight converts to 75.2 g/m², matching standard 75 GSM copy paper (Hammer-IMS).
How much water and energy are required to produce one metric ton of paper?
Net fresh-water intake and total kilowatt-hour consumption per metric ton of finished paper vary by paper grade, pulping integration, and white-water loop closure. Steam drying and electrical refining account for up to 30% of a mill’s production costs (NC State BioResources). Nearly 100 metric tons of process water circulate per ton of dry fiber at the wet end before closed-loop recovery and reuse (Oklahoma State University Extension). Pressing removes water mechanically and uses much less energy than evaporation in the dryer section, so greater press-section dryness reduces steam demand.
What is the boundary between paper and paperboard?
EN ISO 536:2020 specifies grammage measurement for paper and board, while commercial conventions distinguish paper and paperboard by structure, stiffness, and end use as well as grammage. In general commercial practice, single-ply or multi-ply webs above roughly 225 to 250 g/m² are commonly grouped as paperboard for folding cartons and linerboard (Wikipedia). (Wikipedia).
References & Sources
- Oklahoma State University Extension (Salim Hiziroglu), Basics of Paper Manufacturing (Fact Sheet FAPC-169) covers topics such as chemical composition of wood, chemical vs. mechanical pulping yield and wet-end stock dilution.
- NC State University BioResources (Hubbe et al.) covers topics such as mineral filler ash loading and inter-fiber hydrogen bonding in Prospects for Maintaining Strength of Paper and Paperboard Products While Using Less Forest Resources: A Review.
- NC State University BioResources, Energy Efficiency Challenges in Pulp and Paper Manufacturing: A Tutorial Review — dry-solids progression across forming, pressing, and thermal drying and up to 30% mill energy cost share.
- NC State University BioResources covers topics such as Crescent Former and Yankee cylinder creping effects on 13 to 35 g/m² tissue in Understanding the Effect of Machine Technology and Cellulosic Fibers on Tissue Properties: A Review.
- U.S. Environmental Protection Agency (EPA), Paper Recycling Frequent Questions practical wood cellulose fiber recovery span and virgin fiber reinforcement.
- Hammer-IMS, Understanding Basis Weight Measurement in Paper — North American parent sheet conversion table (20 lb Bond = 75 g/m², 50 lb Text = 74 g/m²) and ±5% US GPO tolerance.
- PaperIndex Academy, Diagnosing Packaging Failures: Why Paper Bags Tear During Delivery >50% tensile drop at 15%–20% moisture and +15% cost impact of upgrading 80 GSM to 100 GSM.
- Fortune Business Insights, Pulp and Paper Market Size, Share & Industry Analysis (2026–2035, Report FBI103447) USD 351.70B (2025), USD 357.60B (2026), USD 416.56B (2035), 1.7% CAGR, and 56.40% Asia-Pacific share.
- Stibbe, The Amended EUDR: What Has Changed and What Has Remained? Regulation (EU) 2025/2650 enforcement dates (30 Dec 2026 / 30 Jun 2027) and Annex I scope (HS Chapters 47 & 48 retained, ex Chapter 49 removed).
- Packaging Digest, High-Barrier Material Takes Paper Packaging to a New Level — recycle-ready high-barrier paper food packaging structures.
- WIPO Patent Publication WO2026024493A1, Metallized High Barrier Paper Food Packaging 75% WVTR reduction (0.021 g H2O/100 in²/day) and 90% OTR reduction (0.0463 cc O2/100 in²/day).
- PrintPlanet Practitioner Forum, Grain Direction in Commercial Printing and Folding — machine-direction vs. cross-direction folding behavior.
- Encyclopædia Britannica, Paper: Definition, Papermaking, & Facts historical evolution from Cai Lun (105 CE) to Fourdrinier machines.
- Wikipedia, Paper — general cellulose web overview, historical timeline, and ISO 216 / ANSI sheet standards.
Reviewed by the Henan Zejiang Paper Machinery Co., Ltd. technical team.