Get in touch with Zejiang Paper Machinery Company

Updated August 2026
Paper machine parts are the individual components, headbox, forming fabric, press rolls, dryer cylinders, doctor blades, and Yankee cylinders among them, that move stock through a paper machine from wet end to reel, each one removing water or shaping the sheet before handing it to the next section. Sourced as paper machine spare parts, they only make sense as a system. Search for a single component in isolation, a headbox spec sheet, a doctor blade material chart, and you get an answer to a narrow question. But a worn press felt, a mismatched doctor blade, or an undersized dryer cylinder rarely fails on its own; it shows up as someone else’s problem three sections downstream. This guide walks through the whole machine, wet end to reel, the way an engineer actually has to think about it: what each part does in the broader paper manufacturing process, how a failure in one section becomes a symptom in another, how to tell a genuinely compatible replacement part from a risky guess, and when replacing is worth it versus rebuilding. It’s written from inside the paper manufacturing industry, not as a generic parts catalogue.
Quick Specs, Paper Machine Parts at a Glance
| Part category | Machine section | What it does |
|---|---|---|
| Headbox | Wet end | Distributes dilute stock into a uniform jet across machine width |
| Forming fabric | Wet end | Drains water and knits fibers into the initial sheet |
| Press rolls / vacuum rolls / couch rolls | Forming-to-press handoff | Couch roll finishes vacuum dewatering on the wire; press and vacuum rolls then squeeze out more water mechanically under nip load |
| Press felt / dryer fabric | Press & dryer sections | Carries the sheet, absorbs/releases pressed water, holds it against dryer cylinders |
| Dryer / Yankee cylinder | Dryer section | Steam-heated pressure vessel that evaporates remaining moisture |
| Doctor blade | Press / dryer / calender / Yankee | Cleans rolls, sheds the sheet, conditions the surface — the one part that runs everywhere |
| Refiner plates / screen baskets | Stock-prep (upstream) | Fibrillates and screens pulp before it ever reaches the headbox |
What Paper Machine Parts Actually Do, Anatomy From Wet End to Reel
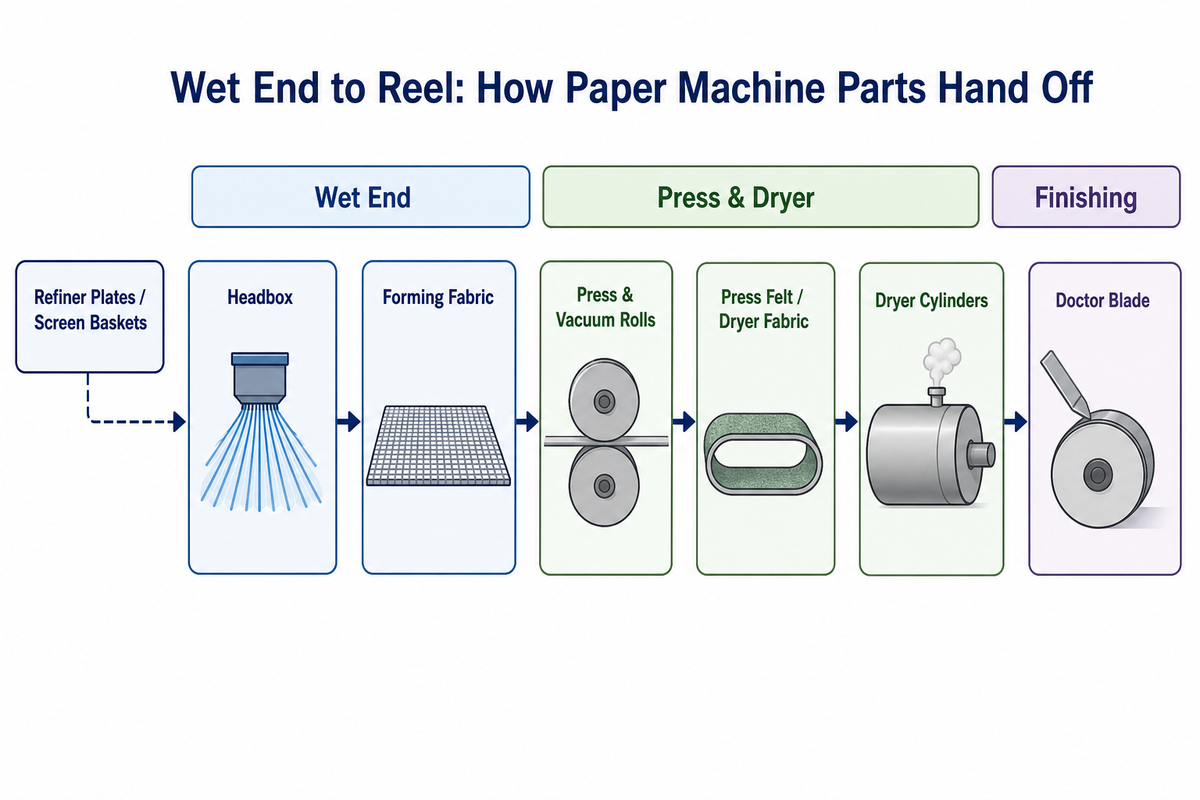
A paper machine is a sequence of dewatering and drying stages, and each of the parts of paper machines exists to solve exactly one problem in that manufacturing process before handing the sheet to the next section. Stock, dilute paper pulp, typically well under 1% consistency at the headbox, leaves the reel as a finished paper sheet, with every part in between removing water either mechanically or by evaporation.
The headbox spreads that slurry into a uniform, controlled-velocity jet across the full machine width; a mismatch between jet speed and forming-fabric speed shows up later as fiber misorientation and uneven strength. In the forming section, the forming fabric drains the first and cheapest water out by gravity and a series of suction boxes under vacuum. A couch roll, the last vacuum-dewatering point on the wire, hands the sheet off to the press section, where press and vacuum rolls squeeze out the next stage of water mechanically under nip load, dewatering here’s far cheaper than evaporating the same water later. What the press section doesn’t remove becomes the dryer section’s problem: a train of steam-heated cylinders, each one a pressure vessel, that evaporates the rest. That designation carries real regulatory weight, though not always cylinder-by-cylinder: Delaware’s pressure vessel code, for instance, groups “rolls of a paper machine or a dryer operating as a single machine or unit” together as a single regulated pressure vessel rather than certifying each cylinder separately, and Washington State’s boiler law separately references TAPPI TIP 0402-16 for paper machine dryers specifically. In the United States, the current ASME Boiler and Pressure Vessel Code (2025 edition) is the baseline most manufacturers build dryer cylinders to; other markets apply their own equivalent, such as the EU’s PED or China’s TSG/GB codes. The doctor blade is the one part that shows up in almost every section, press, dryer, calender, and (on tissue lines) the Yankee, cleaning roll surfaces and shedding the sheet at each stage.
One boundary worth stating up front: refiner plates and screen baskets belong to the stock-preparation line, upstream of the paper machine itself, not to the machine sections covered here in depth. See the boundary note below for where to go deeper on that category.
Each part category above has its own selection logic, spec ranges, and OEM-compatibility questions: see headbox types and specifications, press, vacuum & couch rolls, dryer & Yankee cylinders, forming fabric, press felt & dryer fabric, and doctor blades for full spec ranges and selection matrices, or start from the paper machine parts hub to browse the full catalog by section.
The Wet-End-to-Reel Fault Trail, How One Worn Part Becomes Another Section’s Problem
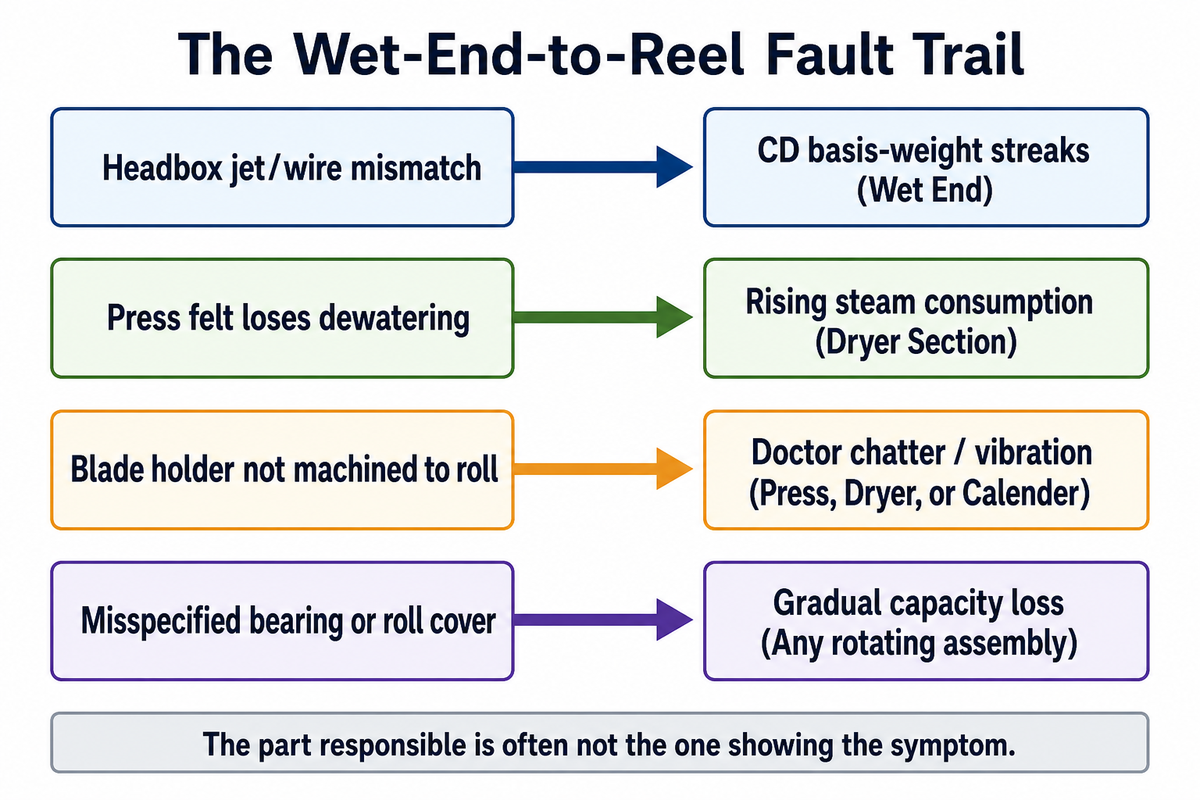
If your machine is slowing down or your paper has a defect, the part actually responsible is often not the one showing the symptom. Sections hand problems downstream, and by the time a symptom is visible it has usually already cost you somewhere upstream. Below, a symptom-to-part table traces the most common fault trails, how a problem in one part category surfaces as a symptom in a completely different one.
| Symptom you see | Section it shows up in | Part most likely responsible | Why |
|---|---|---|---|
| CD basis-weight streaks | Wet end | Headbox | Jet-to-wire speed mismatch or dilution-zone drift skews fiber distribution before forming even finishes |
| Rising steam consumption, no output change | Dryer section | Press felt (upstream) | A felt that stops dewatering re-wets the sheet after the nip, so the dryer has to evaporate water the press should have removed |
| Doctor chatter / vibration | Press, dryer, or calender | Blade holder or roll surface, not the blade material | A holder not machined to the roll’s actual diameter and beam profile creates uneven loading before the blade material is even a factor |
| Gradual capacity loss, no single failure event | Any rotating/conveying assembly | A misspecified bearing or roll cover elsewhere in the line | Component wear is cumulative, not binary — a misspecified part doesn’t always fail outright; it can generate harmonic vibration that damages couplings and seals over months |
| Sheet breaks recurring at one machine position | Wherever breaks recur | Forming fabric or felt at that specific position | Localized fabric wear or contamination creates a repeatable weak point rather than a random break |
| Reduced heat transfer, slower drying with steam pressure unchanged | Dryer section | Dryer cylinder shell condition | At a given steam pressure, wall thickness and condensate removal govern the actual heat flow — a thicker or scaled shell caps drying capacity (directional guidance from a single manufacturer source, not an independently verified industry-wide rule) |
| Uneven crepe or bulk (tissue lines) | Yankee section | Creping blade wear rate, not the Yankee cylinder itself | Inconsistent blade dulling changes the crepe pattern mid-reel even when the cylinder itself is in spec |
| Vibration and safety concern during pressure testing | Dryer section (out-of-machine) | Test medium choice, not the cylinder design | Because a dryer cylinder is a rotating pressure vessel, safety practice favors a hydrostatic (water) test over a pneumatic (air) one for an out-of-machine pressure test — a compressible gas stores far more energy if the vessel fails, the same reason a steam-filled vessel in service is inherently more dangerous than a water-filled one |
| Limitations — what this table won’t diagnose: control-system faults, furnish/chemistry shifts, and electrical faults produce similar symptoms but aren’t part failures. If the symptom moves around the machine rather than staying at one position, or if it correlates with a furnish change, suspect chemistry before you suspect a part. | |||
⚠️ When not to trust this table
Symptoms that look identical to a parts failure sometimes trace back to furnish or additive chemistry instead, a sudden switch in recovered-fiber source, a retention-aid dosing change, or a water-loop contamination buildup can all produce the same wire marks or sheet breaks as a worn part. Before replacing anything, rule out a recent process or furnish change; a part swap won’t fix a chemistry problem, and a chemistry fix won’t be found by inspecting rolls.
OEM-Compatible vs. Catalog Parts, What Actually Determines Fit
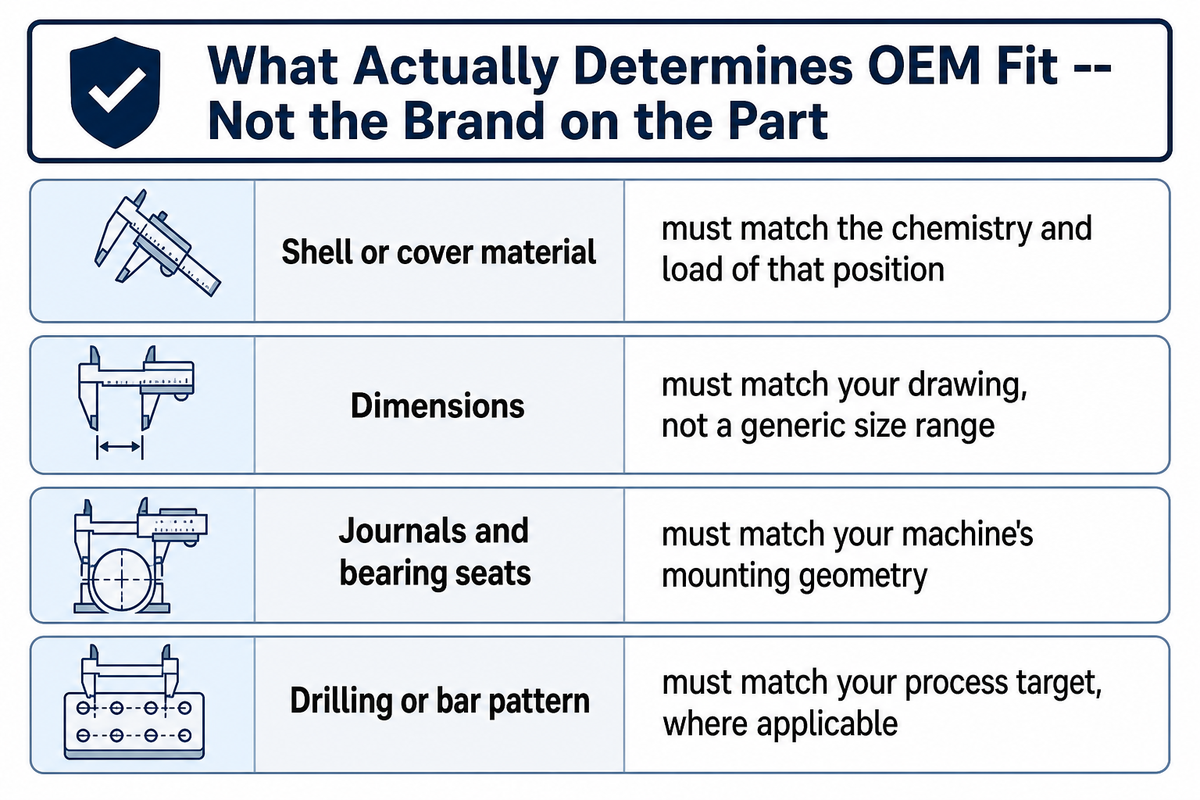
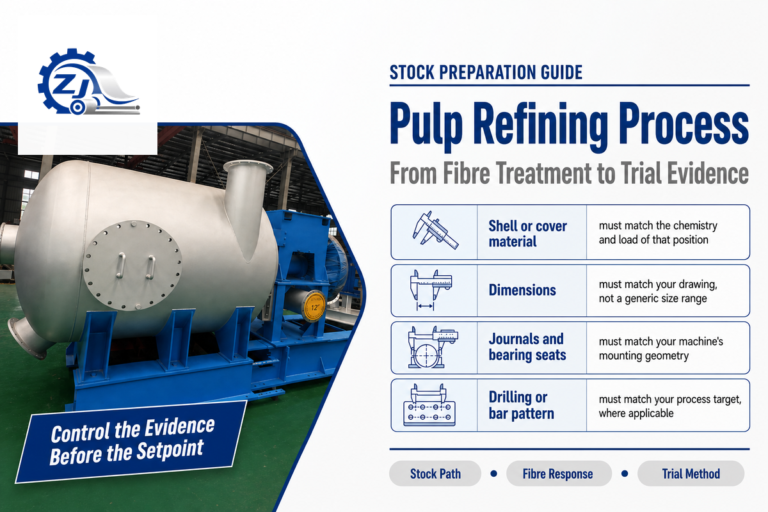
Whether a non-OEM part actually works on your machine comes down to four measurable variables, not the brand printed on it. Shell or cover material has to match the chemistry and load of that position. Dimensions have to match your drawing, not a generic size range. Journals and bearing seats have to match your machine’s mounting geometry. And drilling or bar pattern, where applicable, has to match your process target, not just look similar on a spec sheet.
Brand name is a poor proxy for fit for a structural reason, not as a matter of opinion. Non-OEM manufacturers typically reverse-engineer an original, they buy a part, measure it, and replicate its physical dimensions, without access to the original engineering drawings, material specifications, tolerance stacks, or balance requirements. Small deviations in geometry, material composition, or balance from that process don’t always show up immediately; they surface as accelerated wear or a reliability issue months later. That’s also why the honest answer to “does a non-OEM part void my warranty” is not always, but it can. That risk is real but conditional, not absolute in either direction.
The Cross-Category Fit Baseline — the same four questions, applied to every part category:
| Part category | Primary OEM-fit factor | Secondary fit factor to confirm | New-vs-rebuild signal |
|---|---|---|---|
| Headbox | Type (hydraulic/air-cushion/open) matched to speed and grade | Control integration level (manual vs. DCS/QCS) | Rebuild if slice lips and CD tank are still true |
| Press/vacuum/couch rolls | Shell material + cover compound to nip load and doctor setup | Drilling pattern and lead time on your specified cover material | Re-cover if shell is free of fatigue cracking |
| Dryer / Yankee cylinder | Journal/steam-joint/siphon match to your drawing | Applicable pressure-vessel code for your market | New if shell wall thickness is out of tolerance |
| Forming fabric | Layer construction + mesh count to grade and speed | Endless vs. pin-seam, machine width/circumference | Always new — a consumable, not a rebuild candidate |
| Press felt / dryer fabric | Base construction + batt weight to nip load and dryer temperature | Material (PET/PPS/PEEK) for dryer-zone temperature | Always new — a consumable, not a rebuild candidate |
| Doctor blade | Material family to machine position (see next section) | Holder geometry match to roll diameter and beam | Always new — a consumable, not a rebuild candidate |
| Refiner plates / screen baskets | Bar pattern / slot width to your furnish and freeness target, not brand alone | Custom pattern vs. existing-holder pattern | Always new — a wear consumable |
This is the synthesis none of the individual part pages spell out on their own. Each covers its own category’s fit logic in isolation. Put side by side, the pattern is the same across every category: fit is a function of drawing-level dimensions and duty match, not brand.
“When a customer sends us a worn part or an old drawing, we’re not trying to match a brand name, we’re matching journal diameter, bearing seat, drilling pattern, and shell material to what’s actually installed. A part built to someone else’s catalogue size is a bigger risk than one built to your machine’s real dimensions, no matter whose logo was on the original.”
Wear Parts and Consumables, What to Keep in Inventory
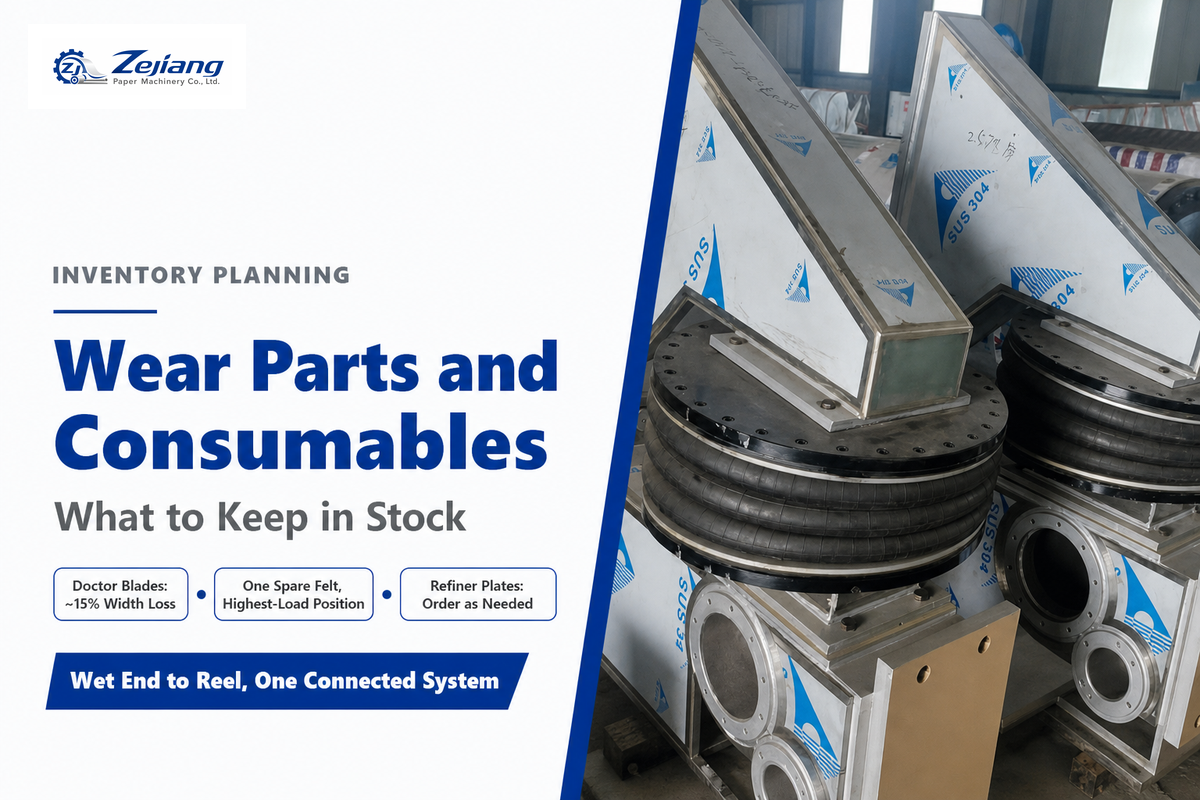
Doctor blades wear faster and more predictably than almost anything else on a paper machine, which makes them the clearest case for stocking rather than reactive ordering. Industry practice is to replace a blade once it has lost roughly 15% of its original width, a figure that’s consistent with published guidance from doctor-system service providers and matches our own product specifications. Waiting past that point risks vibration, edge chipping, and eventually the holder contacting the roll surface directly.
Material selection tracks machine position more than any other variable, wet-end positions call for glass-free, soft blade materials, while press, dryer, and calender positions move toward carbon and ceramic-tipped composites for heat and wear resistance. We cover the full position-by-position material breakdown in our dedicated doctor blade guide; the composite and thermoset blade-material patents cited in References illustrate how far this material engineering has developed.
Inventory rule of thumb: stock doctor blades by position (not a single universal spec), keep at least one full felt/fabric change on hand for your busiest press position, and treat roll covers as a scheduled inspection item rather than a stock item — covers last long enough that pre-emptive stocking rarely pays off.
Several of these categories deserve a note on grade-specific wear. Calendering, smoothing the sheet under load for surface finish and printability, puts a distinct, high-performance demand on doctor blades and roll covers that dryer-section positions don’t share; smoothness targets on coated or fine-paper grades push toward harder, more wear-resistant blade materials than a board machine needs. And a Yankee cylinder producing tissue paper is really just another entry in the same drying cylinders family covered above, with its own creping-blade wear profile layered on top.
✔ Worth stocking
- Doctor blades (by position, they wear on a predictable schedule)
- One spare felt for your highest-load press position
- Common bearing/seal sizes for rolls at frequent-failure positions
⚠ Order-as-needed, not stocked
- Dryer/Yankee cylinders, long lead time regardless, plan around your shutdown window instead
- Forming fabric, grade/speed-specific, custom-cut, not a shelf item
- Refiner plates with a custom pattern, better sourced against your current sample
Where Refiner Plates and Screen Baskets Fit In
Refiner plates and screen baskets belong to the stock-preparation line upstream of the paper machine, not to the wet-end-through-reel sections this guide covers. For bar-pattern selection, alloy classes, and OEM cross-matching, see our dedicated guides on the disc refiner and pulping equipment, and the commercial refiner plates & screen baskets page for current specifications and OEM cross-reference.
We won’t duplicate that selection detail here. In short, bar-edge-length and groove geometry drive refining performance far more than which brand cast the plate does, a distinction that matters more for stock-prep buying decisions than it does for the paper-machine parts covered in this guide.
Fourdrinier vs. Other Machine Types, Why Your Parts List Differs
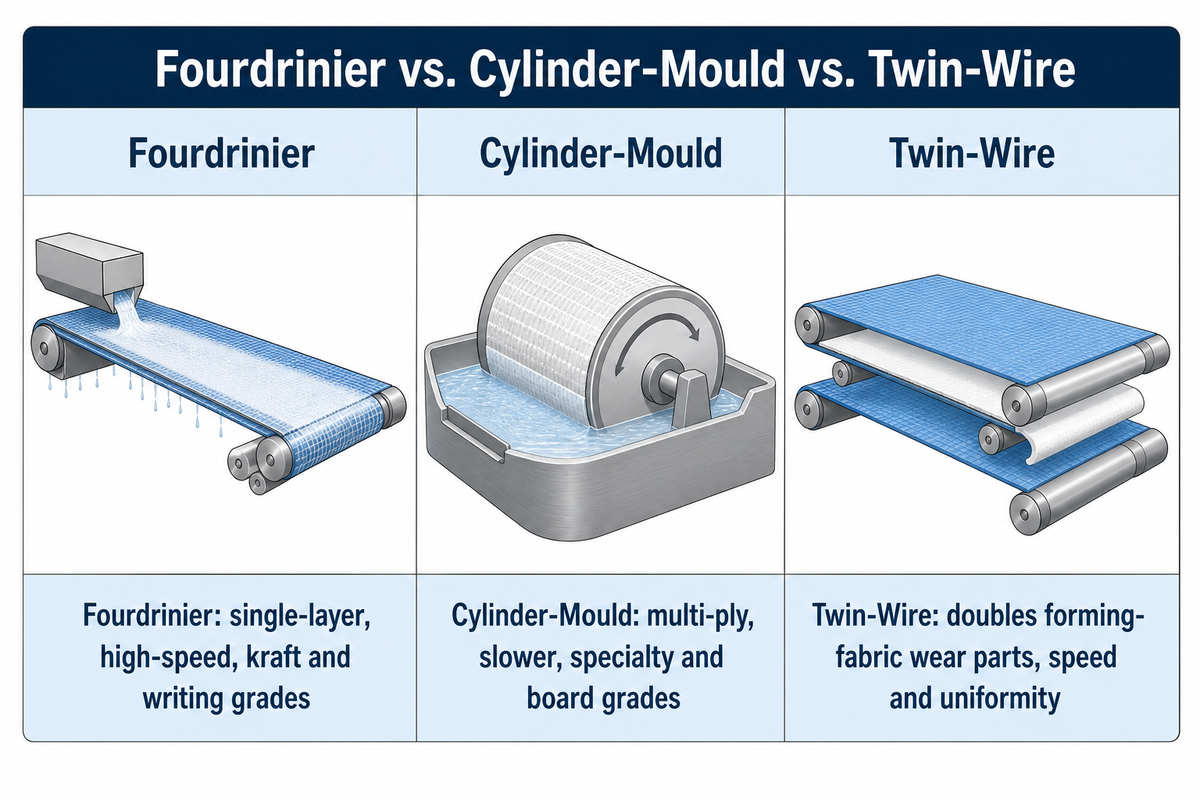
Q: What is a Fourdrinier machine?
A Fourdrinier machine forms the sheet on a continuous flat wire, draining stock by gravity and vacuum as it travels, the standard configuration for high-volume, single-layer grades like kraft and writing paper.
Stock from the headbox lands on a moving flat wire mesh; water drains through the mesh while fibers knit together into a continuous mat. It remains the standard configuration for kraft, writing, and many packaging grades because it handles continuous high-volume production well. A cylinder-mould machine forms each ply on a rotating cylinder partially submerged in a stock vat instead a mechanism that lets multiple plies with distinct compositions be combined wet, which is why it persists for specialty and multi-layer board grades even though it runs slower than a Fourdrinier, and a twin-wire machine sandwiches stock between two forming fabrics to drain from both sides at once, favoring speed and uniformity over a single-wire design. See our Paper Machines Explained guide for the full comparison of forming technologies across machine types.