Get in touch with Zejiang Paper Machinery Company

A turnkey paper mill project is an integrated delivery arrangement that places design and execution responsibilities in one package, but it doesn’t remove the owner’s decisions. The owner still has to specify the result, manage site interfaces, agree what sign-off constitutes acceptance, control change processes, and determine when the plant is ready to be handed over. Poorly defined rules simply create “single responsibility” blind spots.
This guide is for that owner-side work. It doesn’t repeat machine selection, production capacity, equipment configuration, or quotation advice. For those commercial decisions, use Zejiang’s Turnkey Paper Mill Project solution Page. Here the emphasis is on scope control, interface risk, FAT and SAT evidence, punch-list decisions, and a handover package that operators can use.
Five owner controls that run through the whole project
- Requirement baseline: what the completed mill must do and under which agreed conditions.
- Interface register: who supplies each input and who is blocked if it is missing.
- Change control: how design, schedule, test, and commercial effects are approved and recorded.
- Acceptance evidence: what proves a requirement has been met.
- Handover readiness: safety, technical, operational, informational, closeout gates.
What “Turnkey” Changes, and What It Cannot Decide for the Owner
A turnkey package can concentrate design and execution responsibility in one party. This can simplify communication and reduce package-to-package coordination. It doesn’t remove the need for complete employer requirements, accurate site data, approval rights, local permits, input, test rules, or a controlled taking-over decision. The executed contract defines the allocation; the table is a review aid, not substitute contract language.
| Decision | Supplier side | Owner side | Evidence at the boundary |
|---|---|---|---|
| Design basis | Convert approved requirements into an engineered response | Define required outcomes, site facts, constraints, and approval authority | Approved basis document with assumptions and exclusions |
| Battery limits | State terminal points, loads, signals, and supplied items | Provide and coordinate external works and utilities | Interface drawing plus responsibility register |
| Testing | Prepare and perform agreed test procedures | Approve criteria, witness points, and decision rights | Signed protocol, raw results, deviations, and disposition |
| Taking over | Submit completion and turnover evidence | Judge readiness and accept, conditionally accept, or reject | Handover dossier, open-item register, and formal decision |
The ultimate test is simple: for each work package mark “in scope,” ask where it starts, where it ends, what input it requires, what sign-off it depends on, and who approves it? A scope list names the work; a responsibility register links work to sign-off authority.
The Owner’s Interface-Risk Register
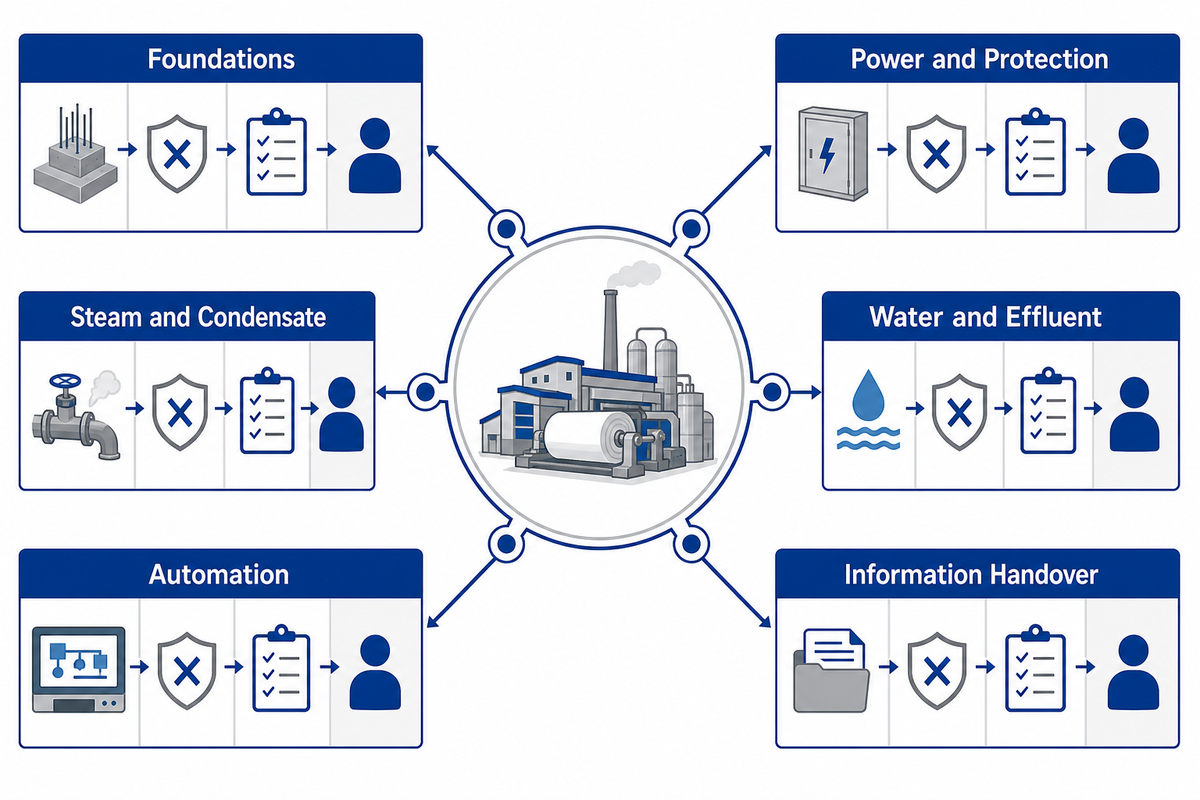
Many costly interface problems aren’t mysterious engineering failures. They’re missing inputs that sit between organizations: a civil load arrives after the foundation is poured, a control signal has no owner, or the wastewater route is assumed to be someone else’s package. An interface-risk register makes those dependencies visible before they become site delays.
| Interface | Upstream input | Downstream decision blocked | Evidence to close | Decision owner |
|---|---|---|---|---|
| Foundations | Soil data, equipment loads, datum system | Foundation release and alignment | Approved load drawing, survey, and as-built record | Owner’s civil lead |
| Power and protection | Supply data, fault level, grounding, settings | Safe energization and drive tests | Approved study, inspection, and energization permit | Electrical authority |
| Steam and condensate | Pressure, quality, flow, return conditions | Dryer readiness and process testing | Tie-in inspection and verified operating data | Utilities lead |
| Water and effluent | Quality, volume, drains, treatment, sampling, permits | Wet testing and discharge readiness | Approved route, operating proof, and permit evidence | Owner’s EHS/utility authority |
| Automation | Signal list, cause-and-effect, network and data ownership | Integrated sequence and fault recovery | Controlled I/O record, logic revision, and test result | Controls lead |
| Information handover | As-builts, manuals, backups, training, spares | Maintainable custody and warranty start | Indexed dossier accepted by operations and maintenance | Plant manager |
Add the stock preparation line, approach flow, headbox, paper machine sections, reel, winder, utilities, building services, laboratory, fire protection, and local-authority interfaces that apply to the real mill. Don’t copy the register unchanged between projects. Its value is in naming the actual handoff and the person who can make the downstream decision.
Hidden Bottleneck Map: “Equipment Complete” Is Not “Plant Ready”
Machine delivered → foundation reference unresolved → alignment can’t close → site acceptance delayed
Controls energized → signal ownership unresolved → integration result is inconclusive → performance evidence delayed
Wet section available → wastewater route or permit evidence unresolved → wet testing can’t responsibly proceed
Trial run complete → software backup, as-built drawings, training, or spares incomplete → operations can’t accept maintainable custody
The rule is that a gate doesn’t advance merely because the upstream party reports completion. It advances when the downstream decision owner accepts the named evidence. This prevents schedule reports from showing false progress while the next team is still blocked.
Freeze Requirements Without Freezing the Wrong Assumptions
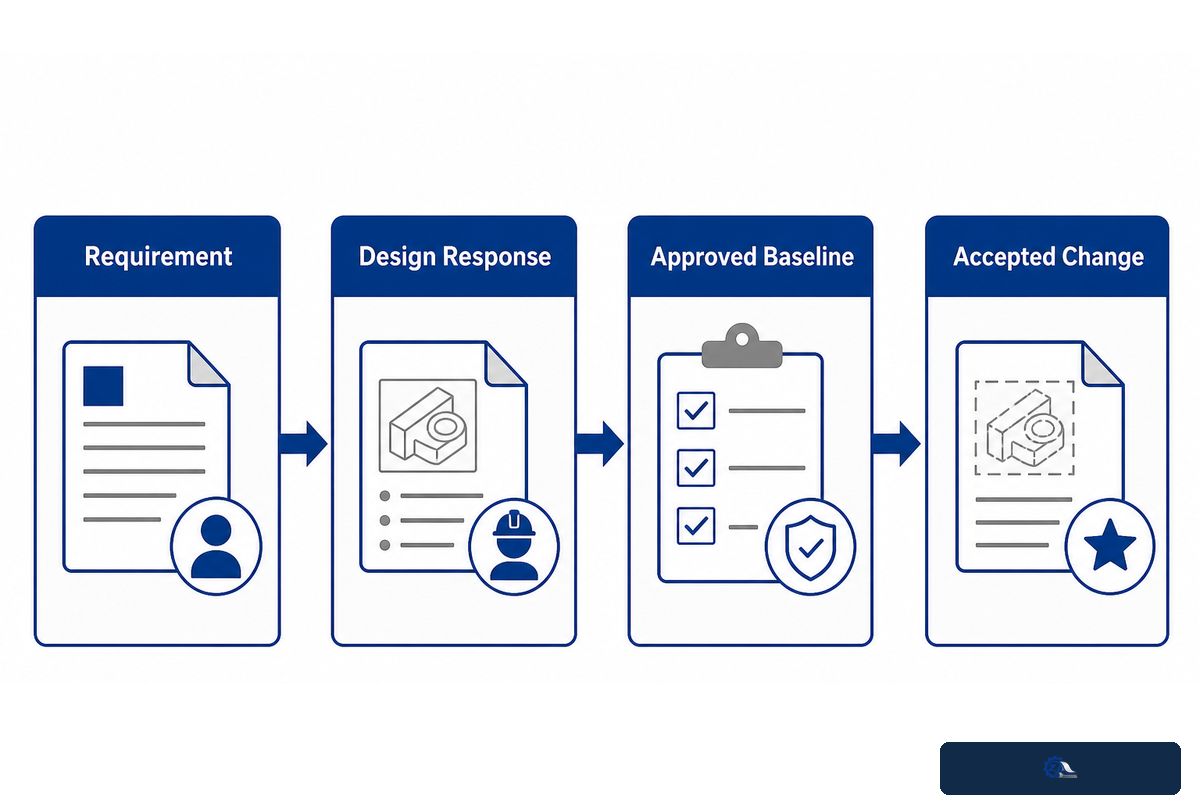
Good project control keeps four things separate that are often mixed together: the owner’s requirement, the supplier’s design response, the approved design baseline, and an accepted change. A supplier drawing can answer a requirement without replacing it. Likewise, a meeting comment can suggest a change without becoming an approved revision.
1. Requirement
What outcome, constraint, or evidence the owner needs.
What outcome, constraint, or evidence the owner needs.
2. Design response
How the supplier proposes to meet it, including assumptions.
How the supplier proposes to meet it, including assumptions.
3. Approved baseline
The controlled revision authorized for execution.
The controlled revision authorized for execution.
4. Accepted change
A reviewed impact, approval, revised document, and closure path.
A reviewed impact, approval, revised document, and closure path.
An effective change request records the reason, affected requirement, safety and permit implications, equipment and interface effects, test impact, schedule and commercial effects, approving roles, revised documents, and closure evidence. If a change alters what will be tested, update the test plan before the test, not after a result becomes inconvenient.
The FAT-to-SAT Evidence Ladder
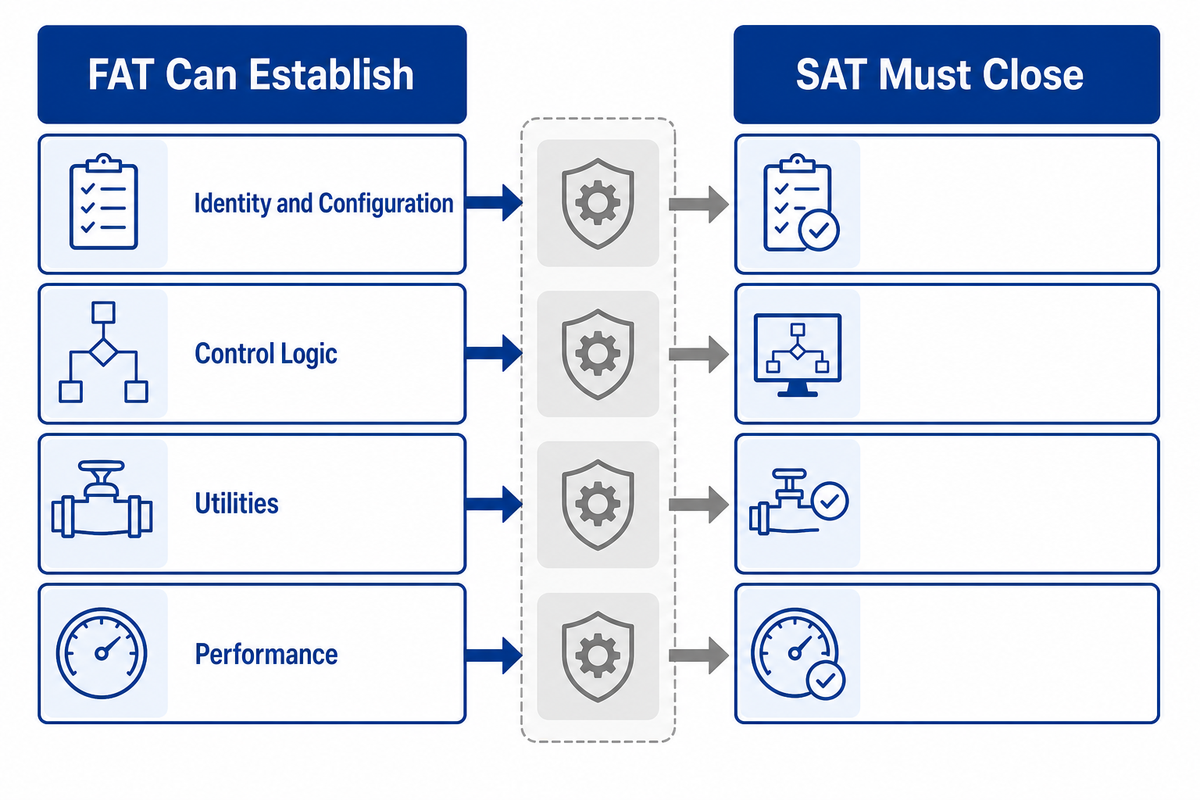
Factory acceptance testing and site acceptance testing answer different questions. FAT can verify agreed equipment, panels, configuration, logic, and simulated functions before shipment. It can’t prove every site utility, installed interface, integrated sequence, or performance condition. SAT closes the site-dependent parts after installation. The exact split belongs in a project-specific test plan.
| Question | FAT can establish | FAT cannot establish alone | SAT must close |
|---|---|---|---|
| Identity and configuration | Installed components and controlled revisions at the factory | Site changes made during erection | As-installed identity and revision reconciliation |
| Control logic | Simulated sequence, alarms, and interlocks | All field signals and real process response | Integrated field behavior and fault recovery |
| Utilities | Specified connection requirements | Actual site quality, stability, and capacity | Verified site conditions at the equipment boundary |
| Performance | Available component or simulated evidence | Integrated paper production under agreed site conditions | Contract-defined result, operating envelope, data, and disposition |
What every test plan should name
- The requirement and configured item being tested.
- The method, instrument, calibration status, and preconditions.
- The representative load, simulation, or operating condition.
- The performer, required witnesses, and decision authority.
- The expected result and acceptance criterion.
- The raw evidence to keep and its file or record identity.
- The deviation, retest, and configuration-control rule.
Evidence strength scale
- The approved requirement and criterion: the question the evidence must answer.
- Traceable certificate or controlled record: useful for identity, conformity, calibration, and documented status.
- Measured result and trend: more powerful when the condition is measurable and the test context is recorded.
- Witnessed functional demonstration: more powerful when behavior, sequence, and recovery must be observed under agreed conditions.
- Photo or verbal assurance: supportive context, not a replacement for measurement when a measurable claim is at stake.
When equipment conditions are measurable, objective measurements and trend records give more convincing acceptance evidence than photographs or verbal assurances alone. More convincing evidence doesn’t mean accumulating more records. It means keeping the evidence that directly answers the agreed decision.
This guide ends before the dry-run, wet-run, first-sheet, and ramp-up sequence. For those operational phases, refer to the paper machine commissioning guide.
Punch Lists, Deviations, and Conditional Acceptance
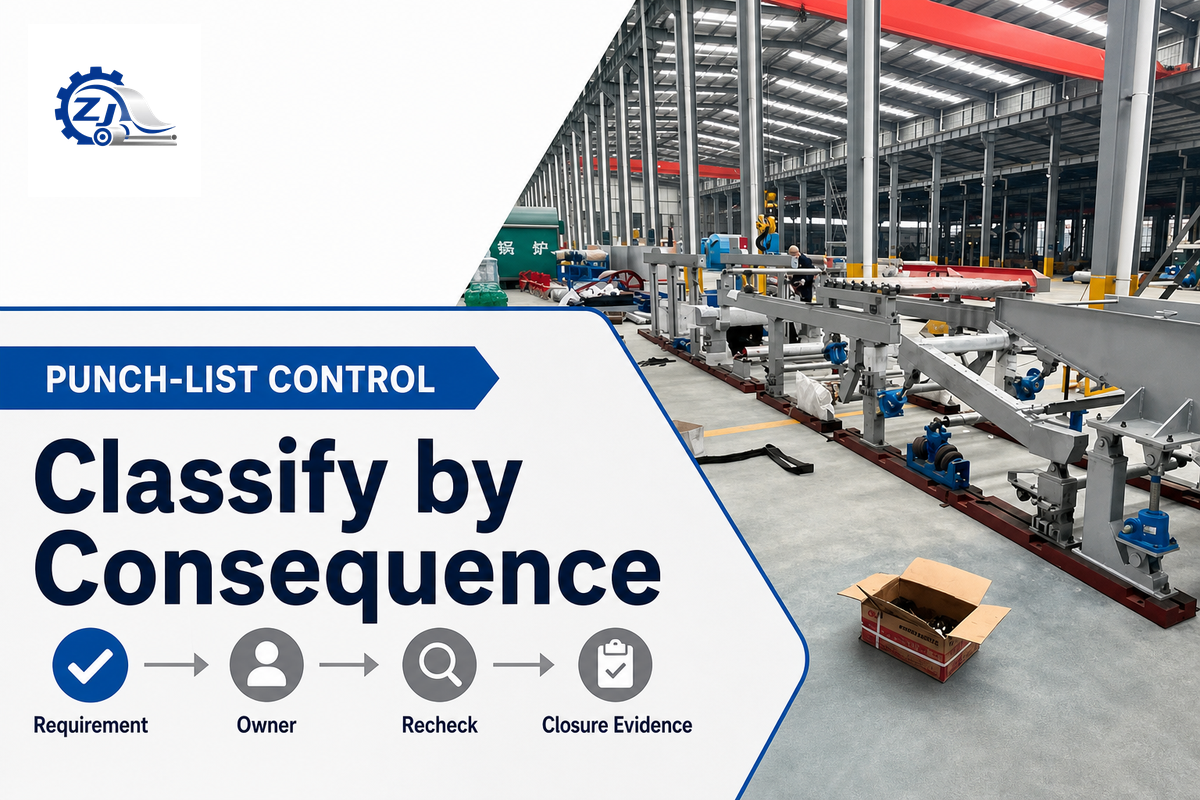
A punch list is only meaningful if each open item is tied to a requirement and a consequence. “Minor” isn’t a technical designation on its own. A label may be cosmetic in one area and a serious isolation error elsewhere. Project-specific categories should be defined before testing and linked to acceptance rights.
| Class | Typical decision significance | Default response |
|---|---|---|
| A | Safety, legal, energization, or environmental blocker | Stop the affected gate until formally closed |
| B | Critical function or agreed performance not met | Correct, retest, and apply contract disposition |
| C | Operability, maintainability, training, or recovery gap | Contain, assign, and obtain operations approval |
| D | Documentation, labeling, or traceability gap | Close with controlled evidence before the relevant milestone |
| E | Cosmetic or minor completion item with no hidden functional effect | Record owner, date, and closure evidence |
Each open item should record the requirement, observed condition, immediate containment, responsible owner, target completion date, recheck method, closure evidence, and consequence on taking over. Conditional acceptance should describe the remaining obligation and remedy. It shouldn’t silently turn a failed requirement into a pass.
The Handover Dossier Index
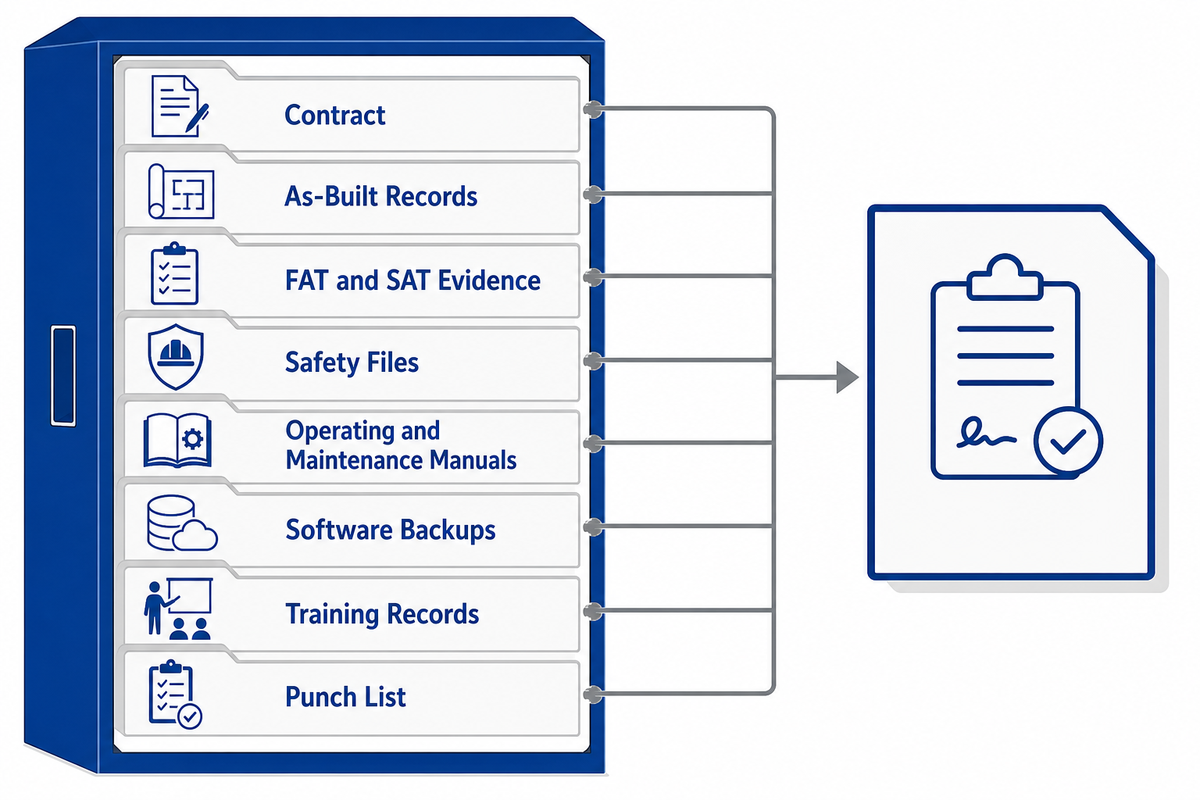
An effective handover file is driven by future decisions, not by the email directories of the supplier. Operations must be able to identify, operate, isolate, maintain, recover, find the limits, understand the risks, and retain warranty evidence for the installed asset.
Ten-folder handover index
- Contract, owner requirements, responsibility matrix, and accepted changes
- Approved design basis, current drawings, and as-built records
- Equipment identity, certificates, configuration, and calibration records
- FAT, integration, SAT, commissioning, deviation, and retest evidence
- Risk controls, isolation boundaries, safety files, and residual-risk information
- Environmental assumptions, permits, wastewater/discharge evidence, and monitoring records
- Operating and maintenance manuals, spare-parts lists, special tools, and warranties
- Software backups, parameters, licenses, access ownership, and restoration instructions
- Training records, operating procedures, and competency handoff
- Punch list, open risks, responsible owners, target completion dates, and closure evidence
The names will differ by contract and jurisdiction. The required outcome doesn’t: the handover dossier should connect approved requirements, current drawings, test records, punch-list status, operating and maintenance information, training, spares, permits, and open-risk ownership to one taking-over decision.
The Five-Gate Handover Readiness Scorecard
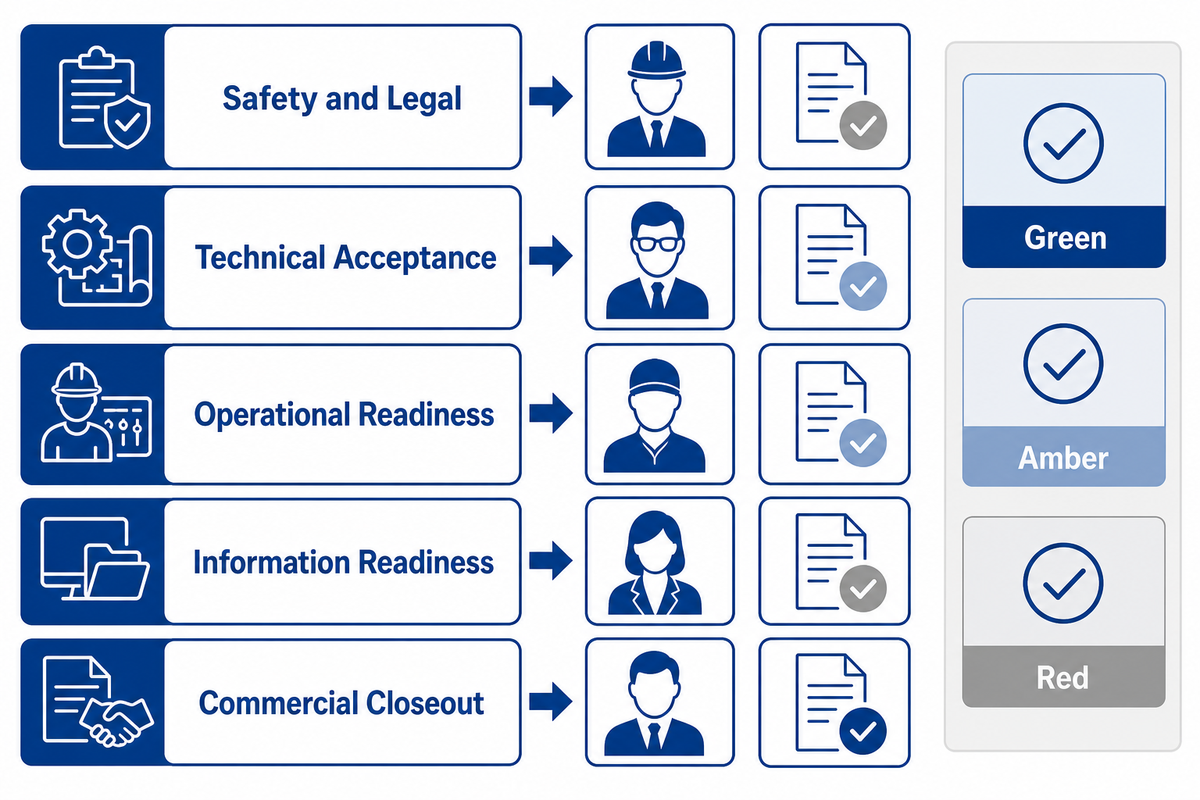
A completion percentage can look reassuring while hiding a critical gap. A gate scorecard asks whether each decision area has enough evidence to move. Use Green, Amber, and Red only after the organization defines who can assign each status. That distinction matters.
| Gate | Pass question | Primary decision roles |
|---|---|---|
| 1. Safety and legal | Are critical hazards, isolations, permits, and statutory holds closed for the intended operation? | EHS, authorized electrical/mechanical persons, owner |
| 2. Technical acceptance | Have agreed tests passed or been dispositioned through controlled deviation? | QA, engineering, commissioning authority |
| 3. Operational readiness | Are people, procedures, utilities, spares, and recovery plans ready? | Plant manager, operations, maintenance |
| 4. Information readiness | Can the plant identify, operate, maintain, back up, and restore what it is accepting? | Operations, maintenance, controls/IT-OT owner |
| 5. Commercial closeout | Are milestone evidence, warranties, open obligations, and release/retention decisions documented? | Owner, procurement, finance, contract manager |
Green: evidence is complete and the authorized decision owner accepts it.
Amber: the open item has containment, owner, due date, closure evidence and a known remedy.
Red: a safety or legal blocker, failed critical requirement, or missing evidence prevents a responsible decision.
Any Red blocks handover. Amber doesn’t automatically permit it; the contract and authorized owner decide whether the residual exposure is acceptable. This is especially important around hazardous-energy control. Commissioning energization and maintenance activities need project-specific isolation boundaries, defined responsibilities, and verification records under the applicable law and site procedure.
Common Owner Mistakes That Create Duplicate Work
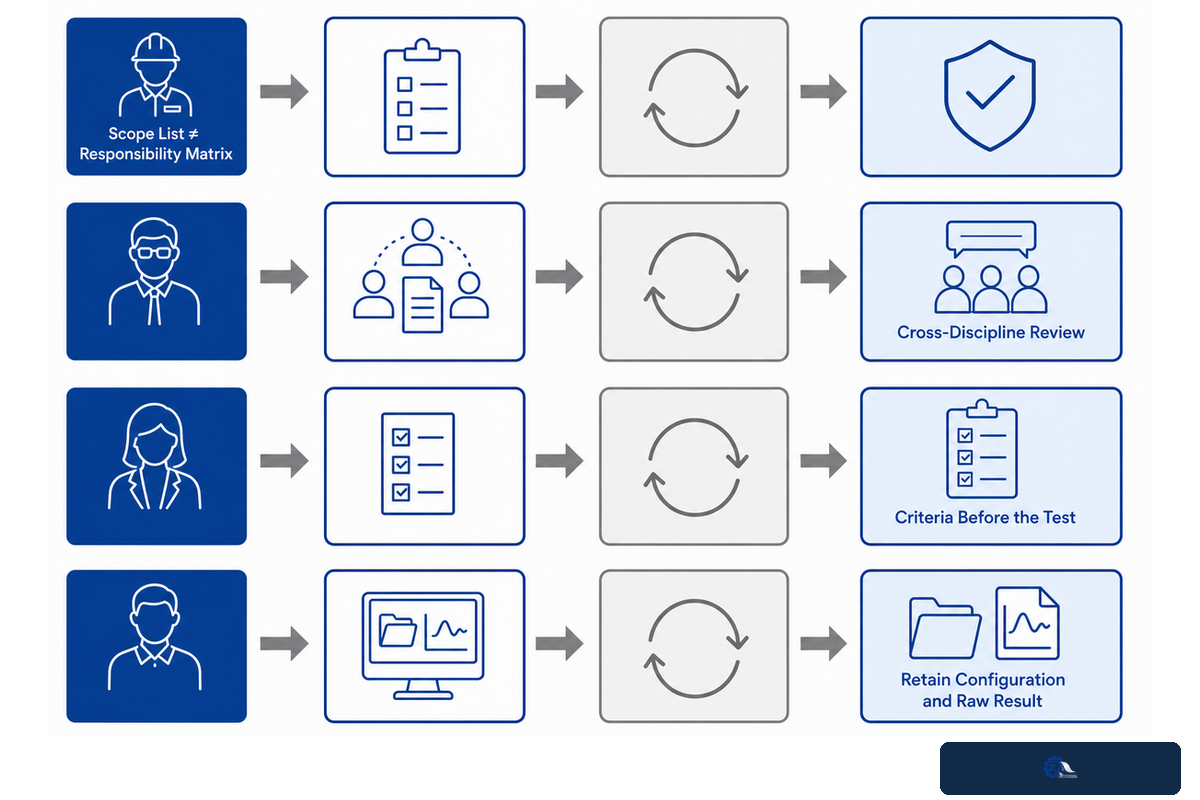
Small shortcuts cause these failures: an unowned interface, an approval without downstream review, or a test with no agreed decision rule. Catching them early costs less effort than repeating civil work, integration tests, training, or handover reviews after the schedule is already under pressure.
- Treating a supplier scope list as a responsibility matrix. The list says what’s supplied; it may not name inputs, interfaces, approvals, or acceptance evidence.
- Approving drawings one discipline at a time. A drawing can be correct inside its package and still fail at the civil, utility, controls, or operations boundary.
- Changing acceptance criteria after the test. This turns a technical decision into a negotiation over results that already exist.
- Witnessing a demonstration without retaining the configuration and raw result. Later teams can’t tell what was actually proven.
- Calling an open item minor without tracing its consequence. Small-looking gaps can block safe isolation, fault recovery, maintenance, or legal operation.
- Accepting hardware while information remains unusable. Missing software backups, as-builts, spares, permits, or training can prevent maintainable custody.
- Using one generic checklist as proof of compliance. Standards, law, permits, contracts, and site rules differ. A checklist helps organize evidence; it doesn’t grant approval.
Frequently Asked Questions
Does turnkey mean the owner has no engineering responsibilities?
View answer
No. A turnkey contractor may carry integrated design and execution responsibility, but the owner still needs complete requirements, accurate site inputs, interface ownership, approvals, test rights, operating involvement, and acceptance authority. The owner also supplies decisions and information that the contractor cannot invent, such as permit conditions, utility boundaries, operating preferences, and who may accept a deviation. The executed contract defines the exact allocation.
What is the difference between FAT and SAT in a paper mill project?
View answer
FAT tests agreed equipment, configuration, logic, or simulated functions before shipment or site integration. SAT closes requirements that depend on the installed equipment, actual utilities, field signals, site conditions, and integrated operation. Neither label defines the whole scope on its own. The project test plan should show which requirement is tested at each location, who witnesses it, what evidence is retained, and what happens if the result fails.
What should be agreed before a FAT starts?
View answer
Agree the item and controlled revision, test method, preconditions, representative load or simulation, instruments, witnesses, expected result, acceptance criterion, retained evidence, deviation handling, and retest rule. Also state which site-dependent questions the FAT cannot close, so a factory pass isn’t mistaken for complete plant acceptance. A visit agenda or demonstration script is useful, but it isn’t a complete acceptance protocol.
Can a paper mill be handed over with an open punch list?
View answer
Possibly, but never by default. Safety, legal, environmental, energization, and failed critical-performance items should remain blockers. Any conditional acceptance needs named residual obligations, containment, responsible owners, due dates, closure evidence, and contract remedies.
Who owns civil, utility, and environmental interfaces?
View answer
The executed contract decides. The interface register should name both the upstream information owner and the downstream decision owner. Wastewater treatment, discharge assumptions, sampling points, and permit evidence belong in that register rather than being assumed complete when equipment is delivered.
What belongs on the commercial solution Page instead of this guide?
View answer
Paper grade, production capacity, process and paper machine configuration, machinery scope, supplier consultation, budget discussion, and quotation belong on the Turnkey Paper Mill Project solution Page. This article stays on owner-side governance and acceptance.
From Project Scope to a Defensible Taking-Over Decision
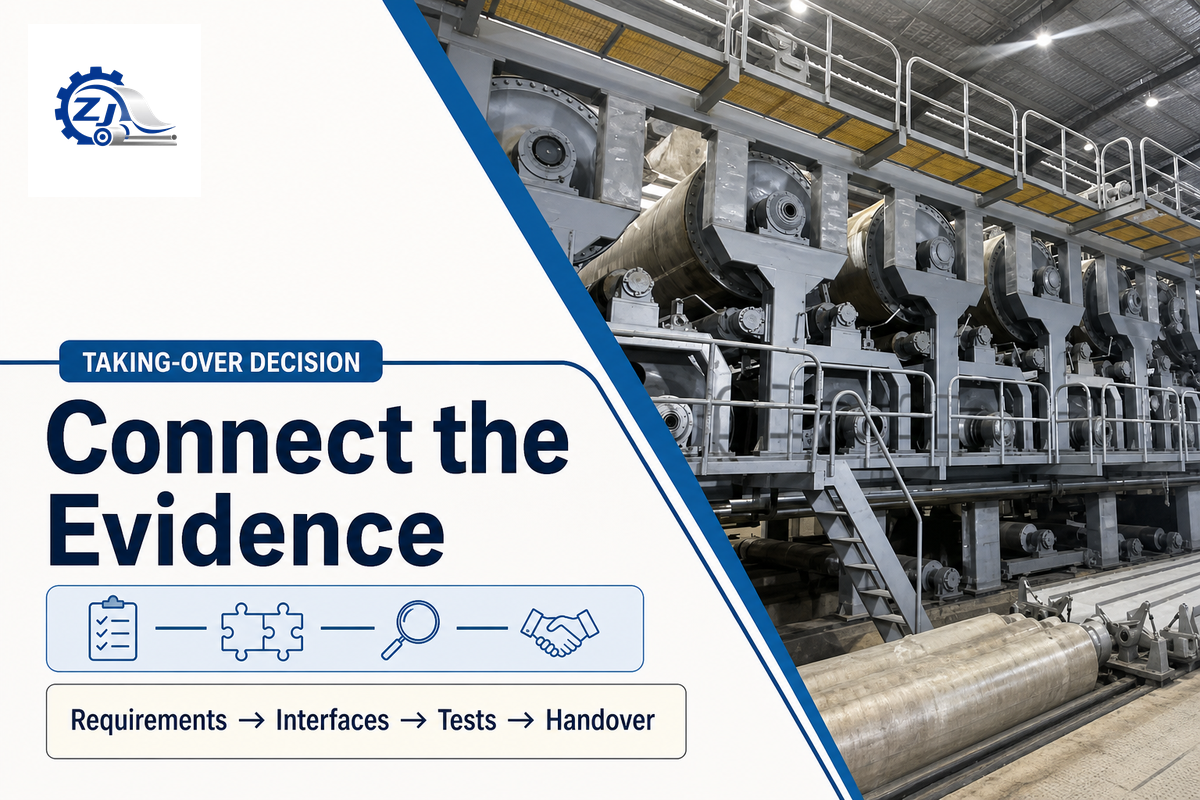
The strongest turnkey project control isn’t a longer checklist. It’s a connected decision system. Requirements lead to controlled design; interfaces lead to named owners; tests lead to retained evidence; deviations lead to explicit dispositions; and handover leads to an authorized decision that operations, maintenance, EHS, procurement, and finance can all trace.
If your requirement baseline is ready and the next step is to discuss paper machine scope, project configuration, or a supplier proposal, continue to Zejiang’s Turnkey Paper Mill Project solution Page. For a project-specific discussion, open the inquiry form.
References & Sources
- IEC 62381:2024—FAT, FIT, SAT, and SIT requirements and checklists for industrial automation systems.
- ISO 21502:2020—project-management guidance.
- FIDIC EPC/Turnkey Contract—employer requirements, testing, taking over, manuals, and as-built documentation context.
- OSHA 29 CFR 1910.147—hazardous-energy control in the United States.
- OSHA 29 CFR 1910.261—United States pulp, paper, and paperboard mill requirements.
- U.S. EPA Pulp, Paper and Paperboard Effluent Guidelines—40 CFR Part 430 context.
- ISO 12100:2010—machinery risk assessment and risk-reduction principles.
These sources support a governance and evidence framework. Local law, permit conditions, the executed contract, approved project documents, and competent professionals control the actual project.
Related resources
- Turnkey Paper Mill Project—commercial scope, configuration, and project inquiry.
- Turnkey Project Scope Checklist—a companion scope reference.
- Paper Machine Commissioning Guide—the operational commissioning sequence.
- About Zejiang Paper Machinery—company background and capabilities.