Get in touch with Zejiang Paper Machinery Company
High-Consistency Pulper for Deinking: Chemistry, Rejects, and the Flotation Handoff

Updated October 2026
Searches for the deinking process of waste paper typically include the same set of steps. However, in a waste paper deinking process, a high-consistency pulper for deinking is part of a stock-preparation system, not an isolated vat. Choose it by checking if the stated raw material can be defibered and conditioned without passing ink, stickies, rejects, water, or hydraulic loads beyond downstream capacity.
This guide covers pulper duty, furnish-specific chemistry, contaminant preservation, flotation or washing handoff, utilities, request-for-quotation inputs, and acceptance evidence. It won’t publish a universal operating recipe, evaluate every pulper design, or replace the broader thickening and deinking process guide. Model selection, quotation and supplier scope remain on the paper pulping equipment page.
High-Consistency Pulper for Deinking at a Glance
A buyer should define seven things before comparing vessels: furnish, required pulper duty, contaminant behavior, downstream separation route, dry-fiber capacity basis, plant interfaces, and acceptance evidence. A proposal that doesn’t define one of these may still have a motor size and nominal output, but it doesn’t describe a comparable deinking duty. The NC State laboratory guide separates pulping, screening, cleaning, washing, and flotation, which is why this checklist treats the pulper as one measured boundary rather than the whole deinking result.
- Name the furnish. Record recovered-paper grades, blend variation, moisture, ash or coating load, wet-strength content, inks, adhesives, plastics, metals, and expected outthrows.
- Define the pulper duty. State what must be defibered or detached at discharge and what will be removed later.
- Protect removable contaminants. Identify the material that must remain large or intact enough for detrashing and screening.
- Fix the downstream route: name the screen, cleaner, flotation, washing, clarification, and thickening boundaries that receive the stock.
- Normalize capacity by comparing dry-fiber throughput, fiber recovery, operating hours, availability, and batch or continuous timing.
- Freeze the interfaces by declaring power consumption, the energy consumption boundary, water, steam, dilution, controls, layout, discharge surge, and sludge responsibilities.
- Agree on proof through a defined furnish sample, sampling points, method edition, mass balance, acceptance metrics, witness points, and retest rules.
These checks change the conversation from “Which pulper is strongest?” to “Which system produces the required handoff with acceptable fiber loss, contaminant debt, and operating burden?” That question can be tested.
What Does a High-Consistency Pulper Actually Do in Deinking?
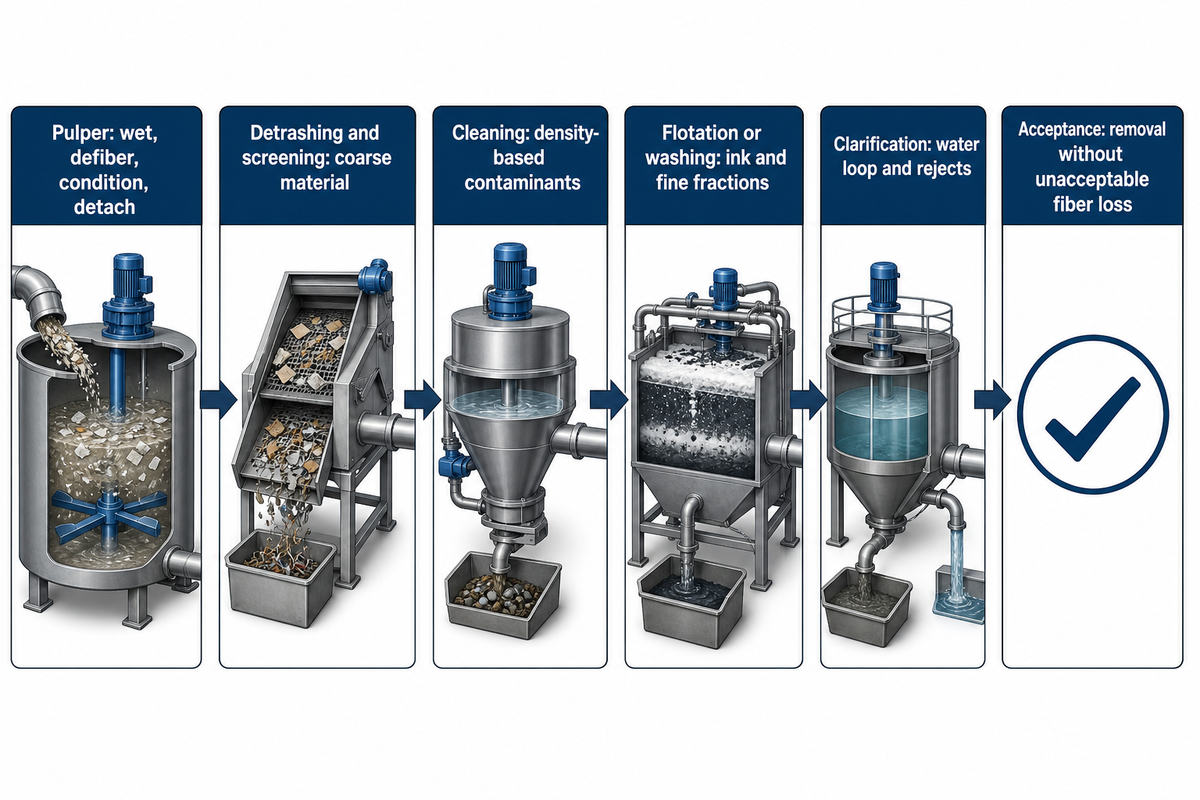
During deinking pulping, a pulper wets and disintegrates recovered paper, promotes fiber separation, and can help detach ink from the fiber surface. Actions commence the pulping process; they don’t prove that detached ink has left the useful fiber stream. Detrashing and screening separate coarse material; cleaning targets density-based contaminants; flotation or washing separates suitable ink and fine-particle fractions; clarification manages the water loop and rejects.
Slushing of recycled paper counts as efficient slushing only when fibers open without turning removable debris into a harder downstream burden.
This accounts for the fact that final brightness can’t be attributed to the pulper solely. A bright sample post-flotation reflects numerous unit operations, chemistry and dilution stages as well as losses. Procurement should instead define a pulper-discharge condition and then track how the stock changes across each downstream step.
| Unit or boundary | Main duty | Useful evidence | What it cannot prove alone |
|---|---|---|---|
| Furnish receipt | Define incoming grades and contaminants | Lot sample, moisture, ash, composition | Pulper performance |
| High-consistency pulper | Wet, defiber, condition, and detach | Flake, discharge, energy, temperature, time | Final ink removal |
| Detrasher or ragger | Coarse contaminant removal | Reject mass and composition | Fine-stickies removal |
| Coarse screen | Separate material at the declared screen plate duty | Accept/reject samples and mass balance | Flotation response |
| Cleaner | Remove heavy and selected density fractions | Feed, accept, reject, pressure condition | All light contaminants |
| Flotation | Carry floatable detached ink particles into froth | Residual ink, dirt, yield, froth reject | Pulper-only detachment |
| Washing | Remove fine suspended material with water | Filtrate load, yield, ash and fines | Universal superiority to flotation |
| Clarification | Condition process water and concentrate solids | Water quality and sludge load | Sheet-quality release |
| Thickening | Remove carrier water and raise consistency | Feed/discharge solids and filtrate | Ink elimination by itself |
“Flotation is the most widely used technology for ink removal in the paper recycling process.”
The practical limit is simple. The pulper prepares a separable suspension; downstream equipment must perform the intended separation without unacceptable fiber loss. Both should be included in the same acceptance criterion.
Build a Furnish-Specific Pulping Window, Not a Universal Recipe
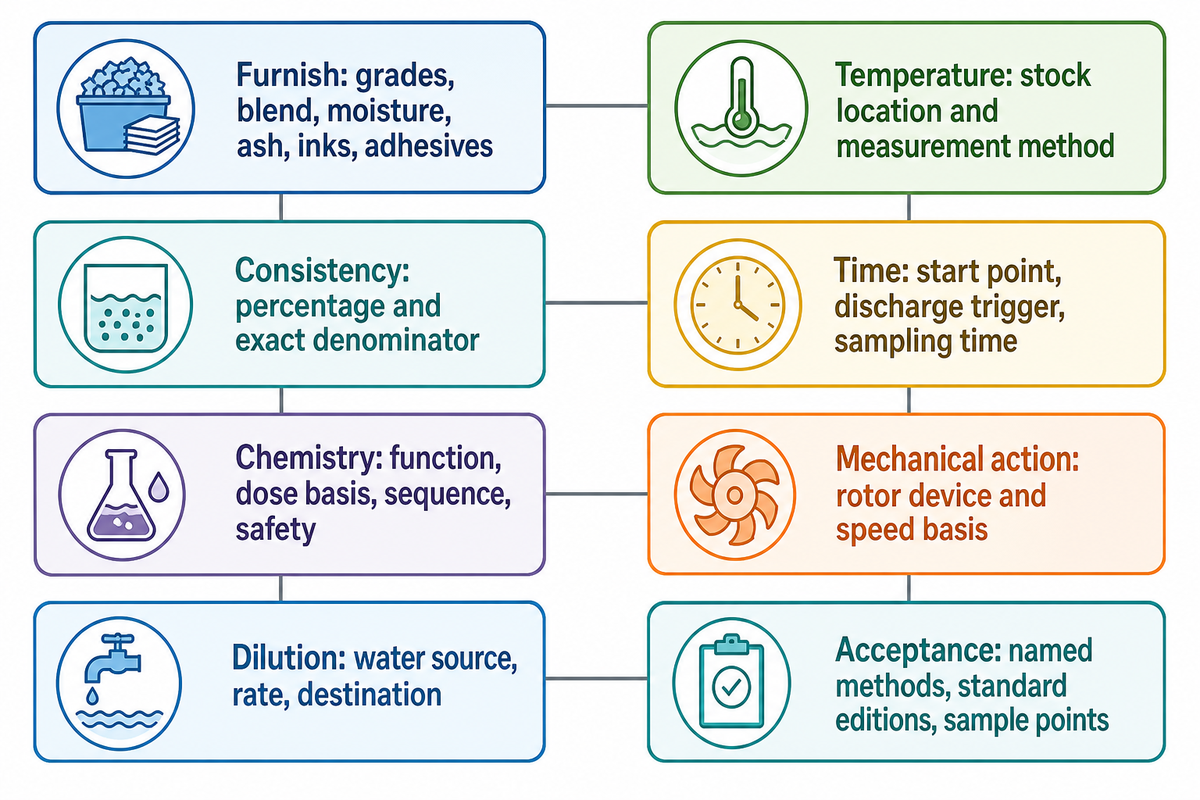
Consistency operation under high concentration conditions alters rheology and mixing; a high-concentration pulp therefore needs a defined basis. Chemistry, temperature, residence time, and mechanical action then interact. Build the starting window from a representative-furnish trial, change one planned factor group, and judge several responses together.
One controlled photocopier-paper study tested chemical deinking at 6%, 8%, 10%, and 12% pulp consistency. Deinking efficiency and ISO brightness rose toward 10% and then declined at 12%; the enzymatic series also peaked at 10% under that study’s conditions. This is a useful counterexample to “more consistency is always better.” It is not a recommendation to run a mill at 10%.
The denominator also matters. INGEDE’s explanation of a revised Method 11 notes that fillers and coating pigment affect rheology and shear. In the cited laboratory context, fiber concentration is fixed at 12%, which means total stock concentration changes with ash. A proposal, therefore, should say whether a percentage refers to oven-dry paper, oven-dry fiber, total solids, or another declared basis.
How should a mill set consistency, chemistry, temperature, residence time, and shear?
Start with a real furnish envelope and measured baseline. Define dose on an oven-dry basis, record ash and moisture, hold sampling method constant, and test defibering, ink behavior, contaminant size, rejects, yield, energy, and downstream separation. Record whether friction between fibers assists opening toward the single fiber state without increasing fiber damage.
| Input factor | Declare before the run | Response to record | Stop or review signal |
|---|---|---|---|
| Furnish | Grades, blend, moisture, ash, inks, adhesives | Lot-to-lot response | Sample falls outside agreed envelope |
| Consistency | Percentage and exact denominator | Mixing, defibering, discharge | Poor circulation or non-comparable basis |
| Chemistry | Function, dose basis, sequence, safety | Ink, yield, water and sludge response | Benefit masks a larger fiber loss |
| Temperature | Stock location and measurement method | Detachment and material behavior | Furnish or additive limit exceeded |
| Time | Start point, discharge trigger, sampling time | Flake, bound ink, reject fragmentation | Marginal gain turns into downstream debt |
| Mechanical action | Spiral rotor or other rotor device; speed basis | Energy and shearing action | Fiber or reject damage rises |
| Dilution | Water source, rate, destination | Hydraulic and process-water load | Downstream capacity is exceeded |
| Acceptance | Methods, editions, sample points | Multi-metric result and mass balance | Result cannot be attributed or repeated |
Treat each deinking agent by function, not as a copied formula. The action of chemicals is influenced by furnish, water loop, dose basis, order, temperature, and ink chemistry. Supplier and mill trials must also review safety and wastewater effects. This supports pulp making decisions before paper making targets are assigned downstream.
The 3-Control Detach-Preserve-Release Framework
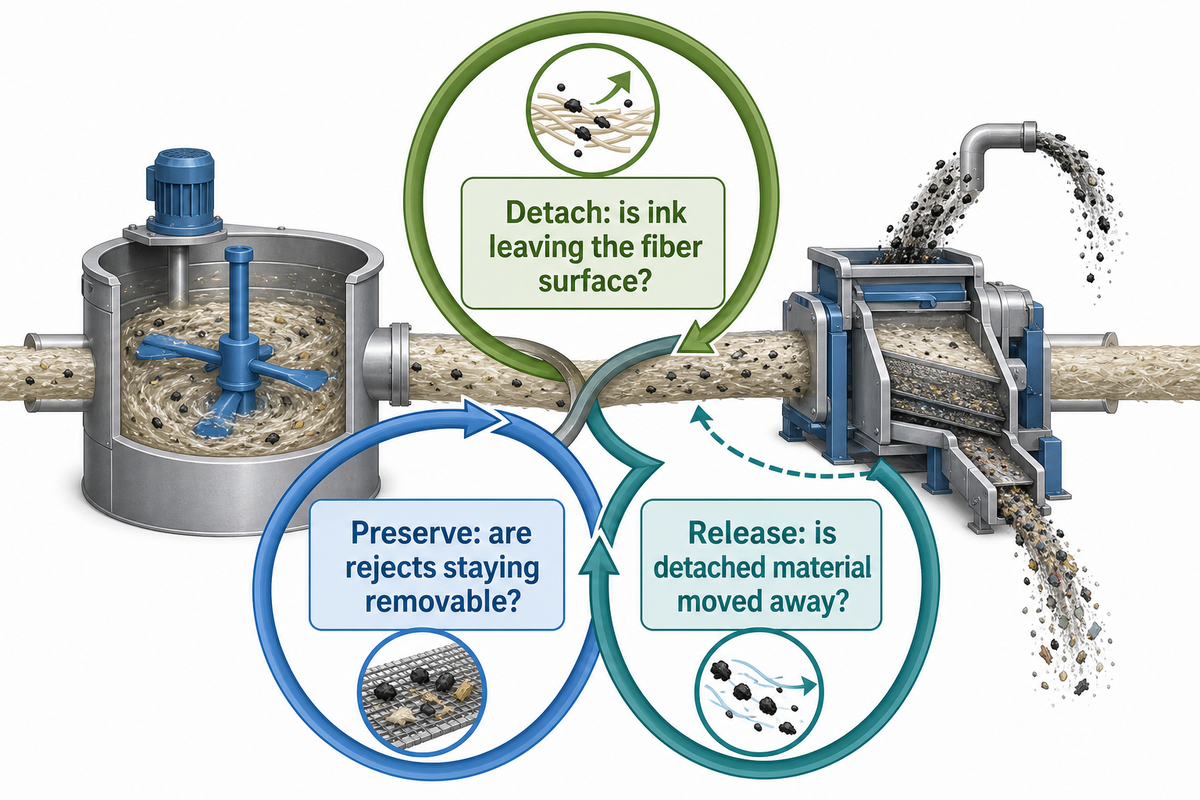
The 3-Control Detach-Preserve-Release Framework audits pulper-to-separation handoff; it isn’t rigidly sequenced. Ink particles and impurities may redeposit, fragment or burden the next interval. Detachment, preservation and release may occur concurrently.
A lab study on a furnish comprised of 80% toner and 20% pigment inkjet showed that micro-scale ink redeposited during conventional pulping. Its fractional route inserted removal between one-minute pulping stages and reduced bound ink under the tested non-chemical conditions. This challenges the assumption to “finish pulping first, remove ink later.” However, the study remains a laboratory case study rather than an industrial design.
| Control | Operational question | Evidence | Failure signal |
|---|---|---|---|
| Detach | Are fibers opening and ink leaving the surface under the stated furnish and chemistry? | Flake or defibering measure, time-bound ink observation | Longer treatment adds little useful release |
| Preserve | Are plastics, adhesives, wet-strength flakes, and other rejects staying removable? | Reject composition and particle-size observations | Coarse contaminants become a fine downstream load |
| Release | Is detached ink or reject material moved away before it redeposits or fragments further? | Free/bound ink where the method permits; reject and water path | Bound ink rises or separation load shifts unseen |
Faster defibering isn’t useful if it turns an easy coarse reject into difficult fines. Complete ink release isn’t achieved if the suspension allows particulate to return to fibers. The goal is to design a system with a measurable handoff, not to strive for maximum activity in the vat.
High-Consistency, Drum, or Low-Consistency: Deinking Handoff Failure Modes
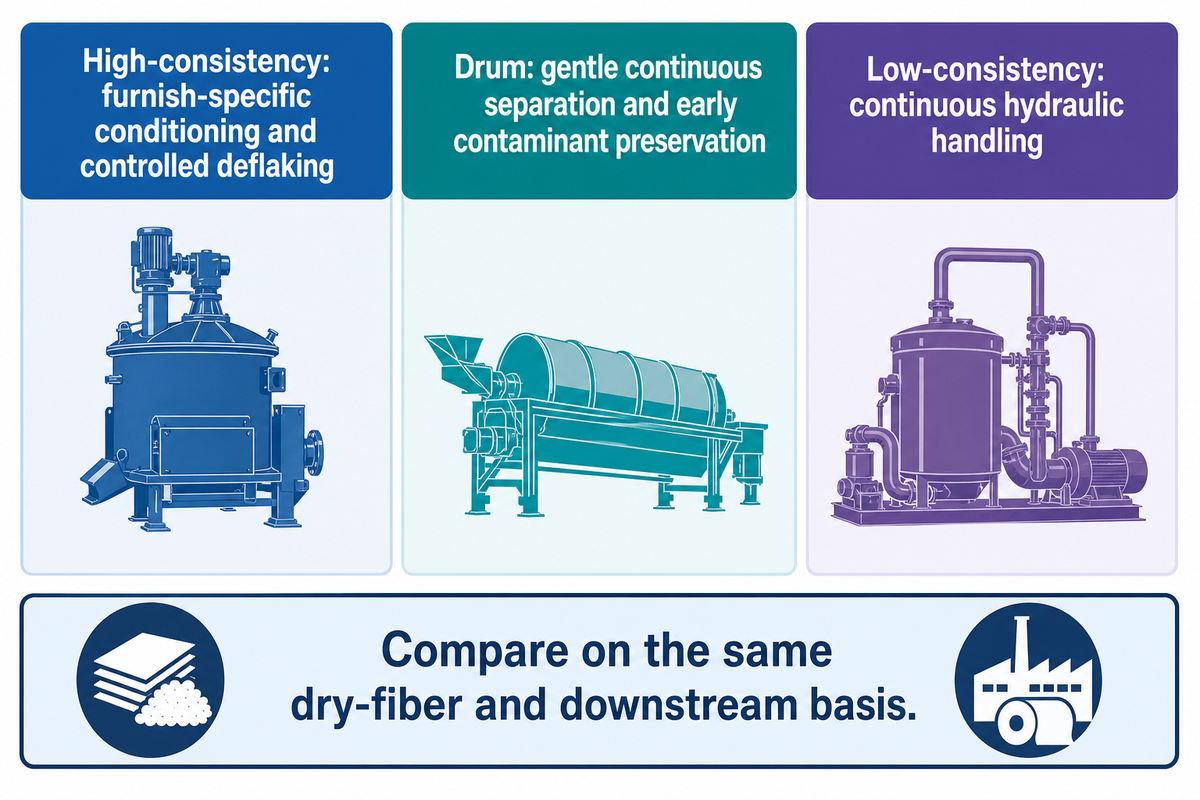
For deinking applications, no reviewed reference places all three types of pulper under a single furnish with similar dry-fiber rates, quality standards, reject limits and downstream line specifications. For generic pulper classification and model comparison, use the published Pulper guide; this section asks only how a route changes ink conditioning, contaminant preservation, fiber loss, and the feed presented to flotation or washing. This screening aid identifies relevant failure modes and evidence. It doesn’t designate an outright winner. A USDA pilot comparison also shows why options need the same yield and quality boundary: similar optical results can accompany different fiber rejection.
When is a high-consistency pulper a better fit than a drum or low-consistency pulper?
Test high-consistency conditions when furnish-specific conditioning, controlled deflaking, and fiber-to-fiber action are central. Test a drum route when gentle, continuous separation and early contaminant preservation dominate. Assess low-consistency duty when the installed line favors continuous hydraulic handling. Compare all options on the same dry-fiber and downstream basis.
| Dimension | High-consistency question | Drum question | Low-consistency question | Evidence to request |
|---|---|---|---|---|
| Furnish | Can the rotor/vat handle its wet-strength and coating load? | Does gentle continuous action preserve its rejects? | Does hydraulic handling fit its debris load? | Same representative lot |
| Operating mode | How are batch time and discharge controlled? | How stable is continuous feed and residence? | How is continuous stock level controlled? | Cycle or residence record |
| Defibering | What discharge measure defines completion? | Which accepts leave without excessive flakes? | What rotor duty reaches the target? | Same method and sample point |
| Contaminants | Which materials may fragment under action? | Which materials leave early and intact? | Which materials enter downstream hydraulics? | Reject audit by family |
| Ink behavior | How are detachment and redeposition observed? | What ink classes need additional conditioning? | What downstream route receives detached ink? | Bound/free ink method where applicable |
| Energy | Can low power consumption be proved at the boundary? | Which auxiliaries are included? | Which pumps and recirculation loads are included? | Metered common boundary |
| Water | Where and when is stock diluted? | What water accompanies continuous separation? | What flow reaches screens and cleaners? | Water and hydraulic balance |
| Rejects | How are ragger/detrasher rejects withdrawn? | How are coarse rejects washed and discharged? | How are light/heavy fractions managed? | Dry reject mass and fiber loss |
| Acceptance | What does the pulper alone guarantee? | What does the drum boundary guarantee? | What does the low-consistency boundary guarantee? | Same furnish, hours, methods, retest rule |
Nominal tons per day can’t normalize options built on different wet-feed, oven-dry, down time and reject assumptions. Any production line quote should state whether paper production capacity or dry-fiber throughput is the governing basis, then restate utilities and acceptance at one boundary.
Protect the Handoff: Rejects, Particle Size, Dilution, and Water
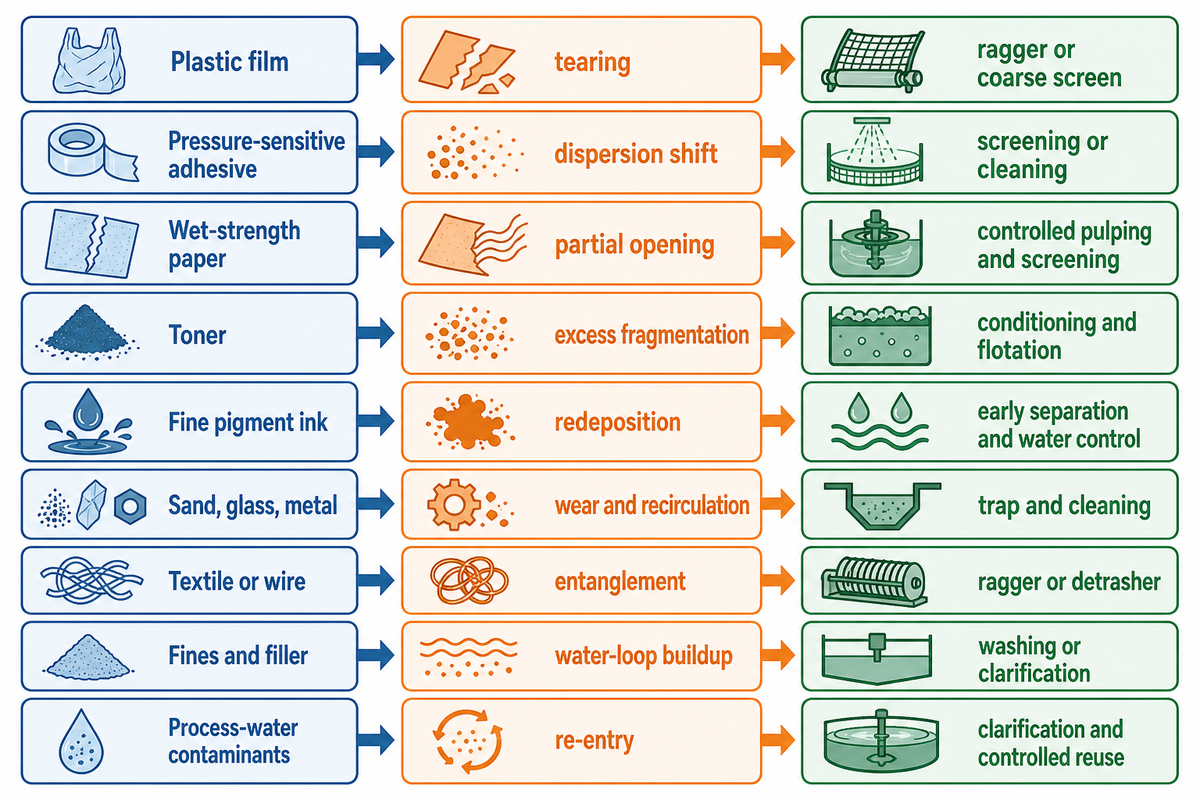
The pulper creates particle-size debt when it turns a removable contaminant into a harder downstream fraction. For this deinking audit, debt means trapped fiber, bound or redeposited ink, dispersed adhesive, wash loss, or a water-loop surge that changes the next separation stage. Good design must recover fibers without shifting hidden debt to pulp quality. Use each row to select paired sample points and a measurement before and after the next deinking unit; this is not a general contaminant-to-exit map.
What must remain intact for downstream removal?
Keep each contaminant within the conditions that the removal step can handle. A nominal or large aperture, by itself, can’t settle the duty because rotor interaction, open area, reject withdrawal, consistency, wear and the next step also matter.
| Material family / state marker | Entry form / ink state | Pulper risk / state change | Planned removal point / deinking observation stage | Evidence at handoff / paired measure |
|---|---|---|---|---|
| Plastic film | Sheets, bags, laminates | Tearing into screen-burdening pieces | Ragger, detrasher, coarse screen | Reject size and fiber carryover |
| Pressure-sensitive adhesive | Labels, tapes, coated fragments | Dispersion or agglomeration changes | Coarse/fine screening, cleaning, dispersion route | Macrostickies method and deposit observation |
| Wet-strength paper | Persistent flakes | Partial opening that traps usable fiber | Controlled pulping and screening | Flake content and reject fiber |
| Toner | Fused printed fragments | Excess fragmentation or fiber entrapment | Conditioning, screening, flotation route | Dirt and residual-ink measures |
| Fine pigment ink | Microscopic particles | Release followed by redeposition | Early/appropriate separation and water control | Free versus bound ink where measurable |
| Sand, glass, metal | Dense particles | Wear and recirculation | Trap and centrifugal cleaning | Heavy-reject audit and wear points |
| Textile or wire | Long, tough pieces | Entanglement around rotating parts | Ragger/detrasher | Withdrawal rate and access record |
| Fines and filler | Suspended small solids | Water-loop buildup and yield loss | Washing, flotation, clarification as designed | Ash/fines balance and filtrate load |
| Process-water contaminants | Returned stickies, pitch, dirt, fibers | Re-entry after the furnish boundary | Clarification and controlled reuse | Fresh/return-water sample locations |
An older trade-press operating account describes both dirty incoming office paper and recirculated process water as contaminant paths. Its age makes it unsuitable for current performance benchmarking; however, the lesson of a path is useful: a stable furnish doesn’t guarantee a stable pulper if the water loop returns stickies, dirt, pitch, rust, sand or felt.
One TAPPI experiment used a 50/50 old-newsprint/old-magazine furnish, pulped at 16% consistency, diluted to about 2% for 1.5 mm coarse screening, and floated at 1%. These are study conditions, not a plant recipe. Their value is the explicit handoff: consistency, aperture, dilution, and component-removal measurements were all named, so the result can be interpreted inside one experiment.
At an equipment level, define pressure-screen duty, pulp cleaning equipment, and deinking and thickening equipment as separate responsibilities. Linking them doesn’t make the guarantees of each interchangeable.
Integration and Utility Requirements Before Layout Freeze
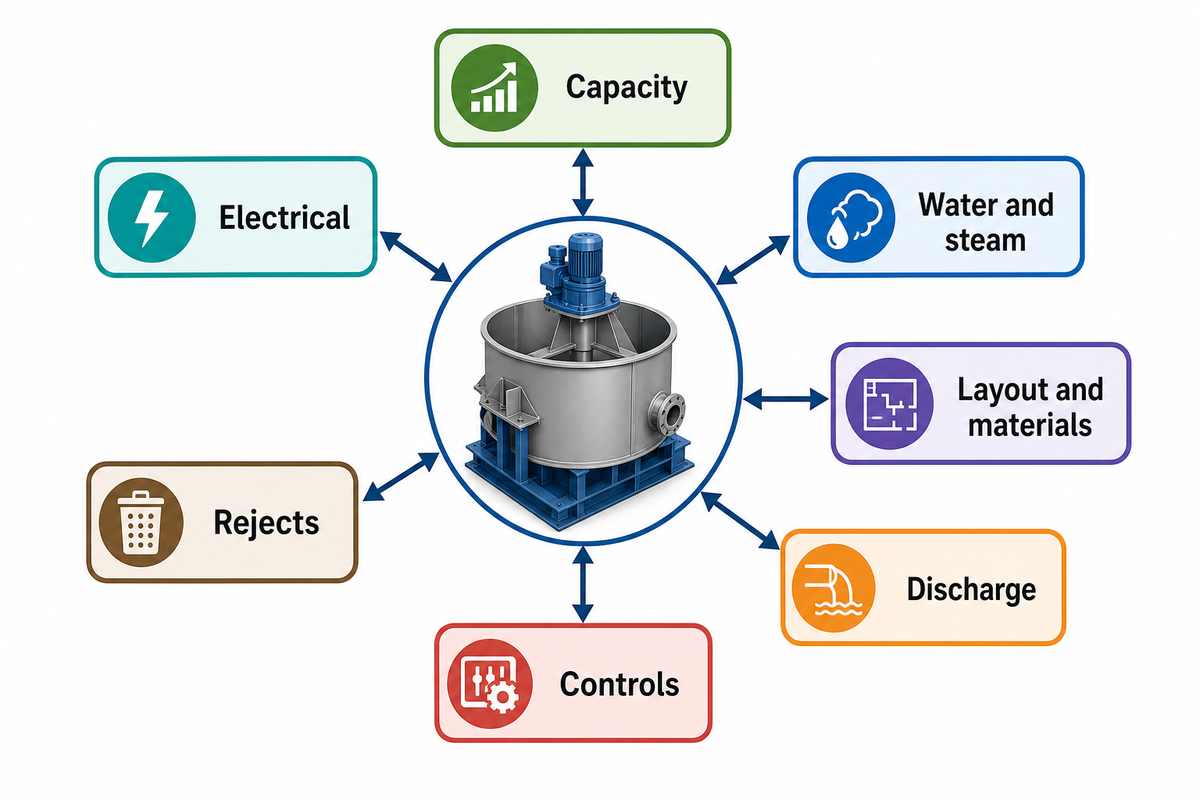
Freeze the system boundary before accepting vessel capacity. A pulper without dilution, discharge, screens, water, power, access, controls, and peak-flow responsibility isn’t comparable. In a new line or upgrade, the transformer, floor opening, stock chest, pump or flotation feed may be the true constraint.
| Interface | Buyer supplies | Supplier declares | Joint check |
|---|---|---|---|
| Capacity | Dry-fiber demand and operating hours | Rated and normal duty basis | Availability and surge margin |
| Electrical | Voltage, frequency, transformer limit | Motor, transmission part, and operating loads | Starting and protection philosophy |
| Water/steam | Quality, pressure, temperature, availability | Use points, dilution water channel, peak demand | Balance and discharge destination |
| Layout/materials | Floor, access, corrosion and wear conditions | Loads, steel plates, stuffing box, clearance | Certificates and removal path |
| Discharge | Downstream chest and hydraulic limit | Discharge system and flow profile | Peak dilution and surge control |
| Controls | Plant system and data requirements | Signals, interlocks, instruments | Cause-and-effect review |
| Rejects | Destination and handling policy | Withdrawal points and expected categories | Washing, dewatering, sampling access |
Compare these interfaces with the broader stock preparation equipment family only after the line boundary is clear. A complete layout drawing should show ownership at every flange, cable, signal, access point, and material discharge.
The Deinking Handoff Dossier: What Buyers Must Specify
A deinking handoff dossier gives every bidder the same furnish, pulper-discharge, chemistry, reject, water-loop, and flotation inputs; generic pulper families, catalog ranges, and price comparison remain with the published Pulper guide and commercial Pulper page. It separates buyer-supplied facts, supplier-declared values, deinking interfaces, factory checks, site process tests, and conditions that trigger a retest.
What should a high-consistency pulper request define for the flotation handoff?
Representative furnish, moisture and ash, dry-fiber capacity, operating schedule, contaminant envelope, target pulper duty, chemical boundary, utilities, reject handling, downstream conditions, controls and materials, documentation, test methods, witness points, and retest responsibility. A model name or wet tons per day alone won’t do.
Copy this table into the request, then replace every “buyer-defined” entry with the mill’s measured data. The format avoids made-up universal ranges.
Deinking RFQ checklist — copy these handoff inputs into the acceptance protocol:
| Parameter | Recommended range, process boundary, or required input | Why it matters | How to verify |
|---|---|---|---|
| Furnish and contaminants | Buyer-defined grade envelope; measured moisture and ash | Establishes the real pulping challenge | Representative retained lots and lab report |
| Capacity and schedule | kg or t oven-dry fiber/h; hours/day; days/year | Normalizes wet-feed and availability claims | Mass balance and guaranteed operating basis |
| Pulper duty | Named discharge condition and sample point | Stops downstream results being assigned to the vat | Agreed flake/defibering and ink observations |
| Chemistry and temperature | Dose on declared dry basis; measured stock location | Prevents hidden recipe and utility assumptions | Trial sheet, safety data, calibrated instruments |
| Utilities and controls | kW, kWh/t dry fiber, water/steam units, signal list | Exposes plant-interface limits | Load list, metering boundary, cause-and-effect test |
| Reject and downstream boundary | Dry reject mass; screen/cleaner/flotation feed conditions | Captures fiber loss and particle-size debt | Accept/reject sampling and hydraulic balance |
| Materials and documentation | Buyer-required wetted materials, drawings, manuals, spares | Supports maintenance and lifecycle review | Document register and material certificates where specified |
| Acceptance and retest | Named method/edition, witnesses, stable-run window, retest rule | Makes the guarantee auditable | Signed protocol and raw test records |
Henan Zejiang paper machinery manufactures and supplies pulping equipment, paper machines, and replacement components. Use the commercial pulping equipment page after the dossier is complete.
Commissioning: Prove the Pulper-to-Flotation Handoff
Mechanical completion and process acceptance address different concerns; mechanical completion checks installation, rotation, guarding, lubrication, instruments, valves, interlocks, no-load operation, and document delivery. Process acceptance asks whether the agreed furnish reaches the defined pulper discharge and downstream handoff without unacceptable loss or contaminant debt.
A USDA pilot comparison illustrates the need for multiple metrics. Under its conditions, a 0.4% chemical charge produced 4.4% oven-dry fiber rejection, while 0.8% produced 7.6%, even though the reported brightness and residual-ink outcomes were close. The metrics do not stipulate a chemical charge; they show that an optical result may mask a yield penalty.
| Evidence group | Record | Acceptance question |
|---|---|---|
| Test boundary | Furnish lot, oven-dry basis, operating window, exclusions | Was the guaranteed duty actually tested? |
| Sampling | Input, pulper discharge, screen accept/reject, flotation or washing points | Can performance be attributed to a stage? |
| Defibering | Flake or agreed discharge method with time | Did the pulper reach its stated handoff? |
| Ink and dirt | Method, edition, free/bound distinction where possible | Was loss caused by non-detachment or redeposition? |
| Mass balance | Feed, accepts, dry rejects, ash/fines, usable fiber | Did cleanliness improve by discarding fiber? |
| Utilities | Metered power, water, steam, dilution, peak flow | Did the installed plant stay inside its interface limits? |
| Repeatability | Stable interval, deviations, witness signatures, raw data | Can the result be reproduced and audited? |
| Retest | Trigger, corrective owner, new furnish criteria, cost responsibility | What happens if the first run is invalid or fails? |
Rather than reproducing a copyrighted test table, write the name of the method owner and edition in the contract. INGEDE maintains methods covering sample preparation, optical properties, macrostickies, ink elimination, incoming paper inspection, deinkability, and adhesive fragmentation. The correct method is dependent on the claim being tested.
In the United States, EPA identifies Secondary Fiber Deink as Subpart I of 40 CFR Part 430 and lists covered deink mill categories; use that current page to prompt a defined process-water, sampling, sludge, and discharge boundary; confirm the applicable jurisdiction independently—this guide is not legal advice.
Frequently Asked Questions
Does a high-consistency pulper remove ink or only detach it?
A high-consistency pulper can promote ink detachment, but downstream separation must remove the suitable detached fraction.
Pulping wets and defibers recovered paper and creates mechanical and chemical conditions that can release ink from fibers. Detrashing and screening remove coarse material; flotation or washing handles selected ink and fine-particle fractions. Because redeposition can occur during pulping, the functions may overlap. Final brightness after the line cannot be assigned to the pulper alone.
What consistency should a deinking pulper run at?
Use a supplier range only as a trial starting point; the workable consistency is furnish-, design-, chemistry-, and method-specific.
Declare whether the percentage is based on total stock, oven-dry paper, or fiber. Then test the actual furnish while recording ash, moisture, rotor/vat duty, chemistry, temperature, time, discharge, contaminant behavior, fiber yield, and downstream response. A controlled study’s optimum or a catalog range is not a universal mill setpoint. Retain the calculation sheet.
Is a hydrapulper the same as a high-consistency pulper?
Hydrapulper is a broad hydraulic-pulping term; high consistency identifies a more specific operating and equipment duty.
Catalogs may say consistency hydrapulper, type hydrapulper, or HC pulper; none of those labels proves duty. Compare the declared consistency basis, rotor and vat configuration, mode, furnish envelope, reject system, discharge condition, and downstream route. Require the bidder to map each label to a measurable discharge and reject boundary.
When should a mill choose a drum pulper instead?
Test a drum pulper when gentle continuous action and early preservation or removal of coarse contaminants dominate the furnish risk.
Compare it with other routes using one furnish, dry-fiber basis, quality target, reject boundary, availability assumption, and downstream line. Do not choose from the machine label alone.
Which chemicals are added during high-consistency pulping?
Chemical programs may include alkalinity, surfactant or collector functions, peroxide systems, stabilizers, and chelation, but the furnish and water loop govern the choice.
Specify every additive by function, concentration, dose basis on dry material, order of addition, stock temperature, contact time, safety requirements, and wastewater effect. Ink technology, coating, ash, wet-strength resin, adhesives, and downstream flotation or washing can change the response. Set a starting plan with the chemical supplier and mill team, then verify it on representative furnish rather than copying a published recipe.
What does a screen basket need to match after the pulper?
Match the basket to contaminant size, stock consistency, hydraulic load, rotor interaction, open area, reject withdrawal, wear, and access.
Also define whether the stage performs coarse or fine screening and which particles must remain removable at that point. An aperture or slot value without the full duty is incomplete.
What information is needed to size and accept a high-consistency pulper?
Provide representative furnish and a shared dry-fiber, interface, reject, downstream, and acceptance basis before preliminary sizing.
The record should cover moisture, ash, furnish blend, contaminants, operating hours, target pulper duty, chemistry boundary, utilities, controls, layout, materials, reject handling, downstream capacity, documents, factory checks, site sampling, method editions, witness points, and retest responsibility. Preliminary sizing compares declared inputs; final process acceptance requires the installed system and agreed test furnish.
Conclusion: Buy the Handoff, Not Just the Vat
The deinking pulper decision becomes defensible once the mill determines what enters, what the pulper must change, what remains removable, where detached material goes, and how fiber loss and utilities will be measured. That system boundary is traceable from furnish through quotations and commissioning.
Key takeaway
Specify a high-consistency pulper on representative furnish, a declared concentration and dry-fiber basis, protected reject pathways, downstream capacity, and multi-metric acceptance evidence; a vessel label and final brightness cannot establish that duty.
Discuss your pulping and deinking duty
References & Sources
- Deinking Recycled Paper through Flotation NC State University laboratory guide.
- Deinking Selectivity (Z-Factor) U.S. Department of Agriculture Forest Products Laboratory.
- Components Removal in Flotation Deinking TAPPI technical paper.
- Optimization of Chemical and Enzymatic Deinking of Photocopier Waste Paper BioResources.
- Fractional Pulping of Toner and Pigment-Based Inkjet Ink Printed Papers BioResources.
- INGEDE Methods to Evaluate Recyclability and Deinkability INGEDE.
- Revised INGEDE Method 11 Available INGEDE.
- Removing Office Paper Contaminants Recycling Today; used for operating-path context, not current performance data.
- Pulp, Paper and Paperboard Effluent Guidelines U.S. Environmental Protection Agency.
Henan Zejiang’s Equipment Perspective
Henan Zejiang Paper Machinery Co., Ltd. supplies paper machines, pulp-processing equipment, spare parts, refurbishment, installation, and technical support for paper mills in international markets. This article uses that equipment perspective to organize buyer questions, but it doesn’t publish customer results, private plant data, or a performance guarantee. A final proposal should be based on the buyer’s furnish, existing line, utilities, and witnessed acceptance protocol.